































































































































































HomeBlog & GuidesGuidesElectrical
End Mill for Aluminum: Square vs Corner Radius, Flute Count
Square or corner radius, 2 or 3 flutes, and which length: how to pick an end mill for aluminum, with every Titan size we stock, priced per piece.
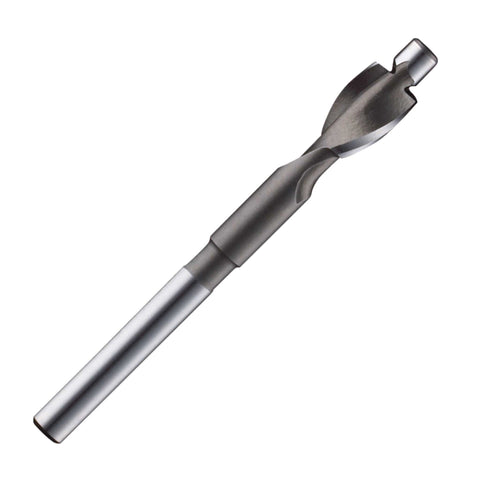
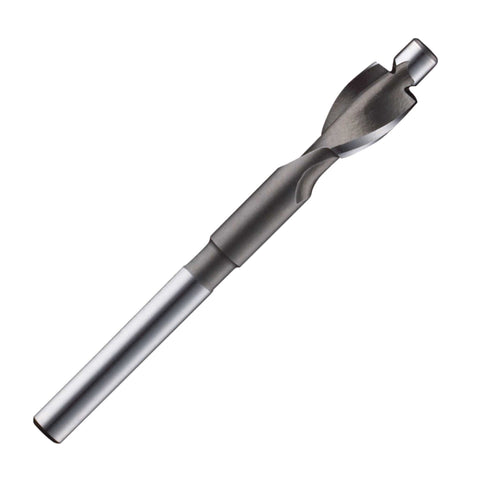
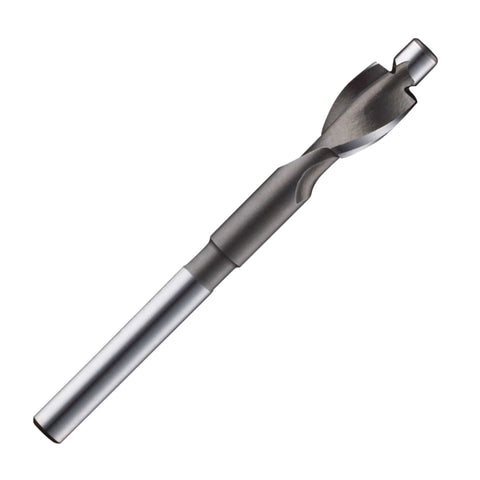
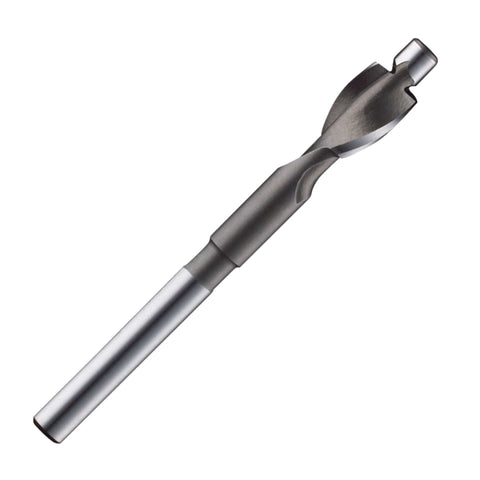
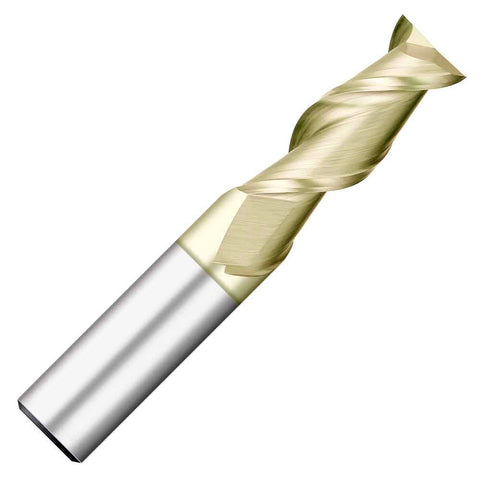
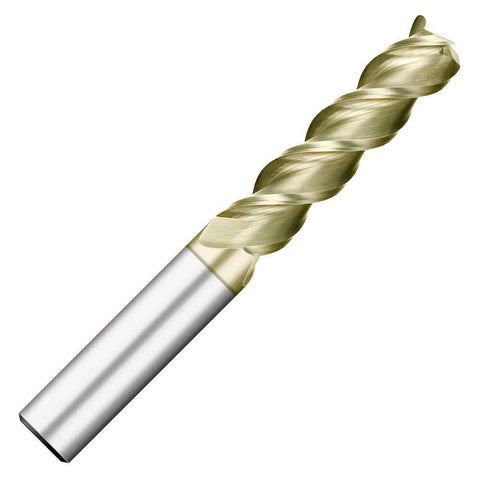
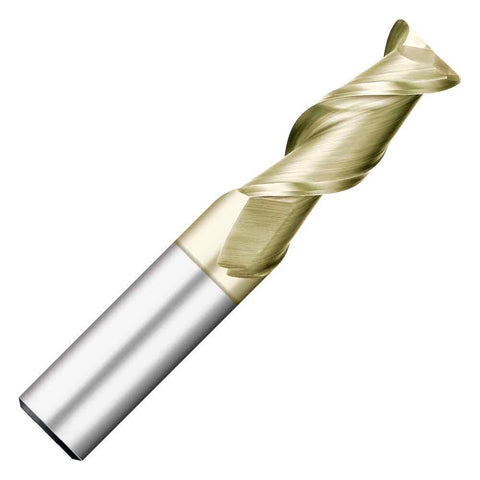
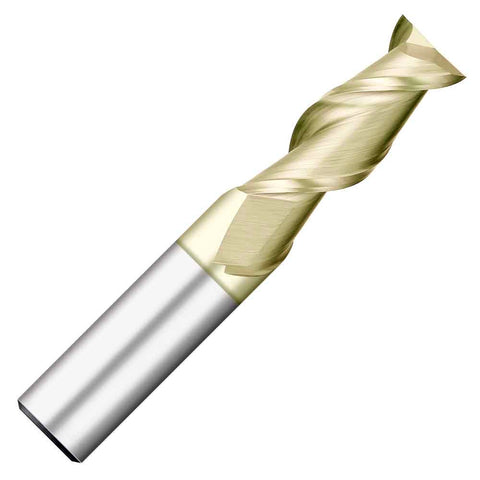
Quick answer: The right end mill for aluminum is solid carbide with 2 or 3 flutes, a high helix and a coating aluminum won't weld to. Every end mill we stock is built that way: Titan USA, 45° helix, ZrN coated, made in the USA. Then make three calls. Corner: square only if the part needs a sharp inside corner, otherwise a corner radius. Flutes: 2 for full-width slots and dry cuts, 3 for pockets and profiles. Length: the shortest that reaches the bottom of the cut.
What makes an end mill right for aluminum?
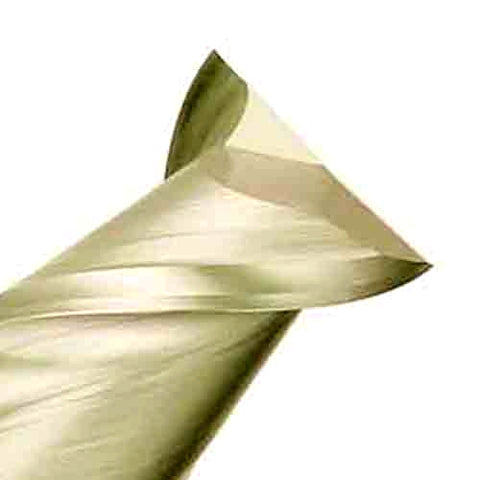
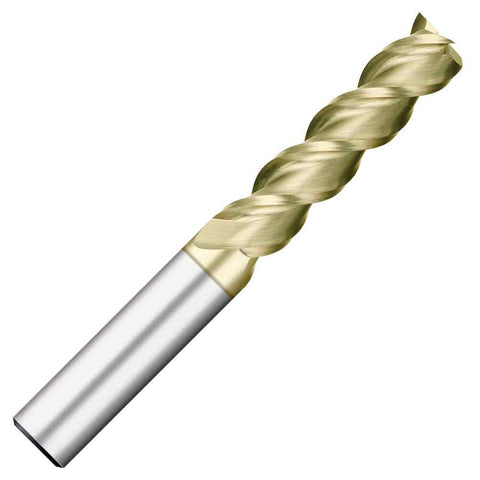
An end mill is right for aluminum when its flutes can throw big, soft chips out faster than the cutter makes them. Aluminum chips are long and gummy. If they stay in the flute, they get cut again, heat up and weld to the edge, and the end mill snaps. Four features stop that:
Few flutes. Two or three, so each gap between the cutting edges is wide.
High helix. A 45° spiral lifts chips up and out of the cut. General-purpose end mills sit nearer 30°.
Solid carbide. Carbide holds an edge at the high RPM aluminum wants.
The right coating. ZrN (zirconium nitride) or bare polished carbide. Skip AlTiN and TiAlN: they contain aluminum, and aluminum chips stick to them.
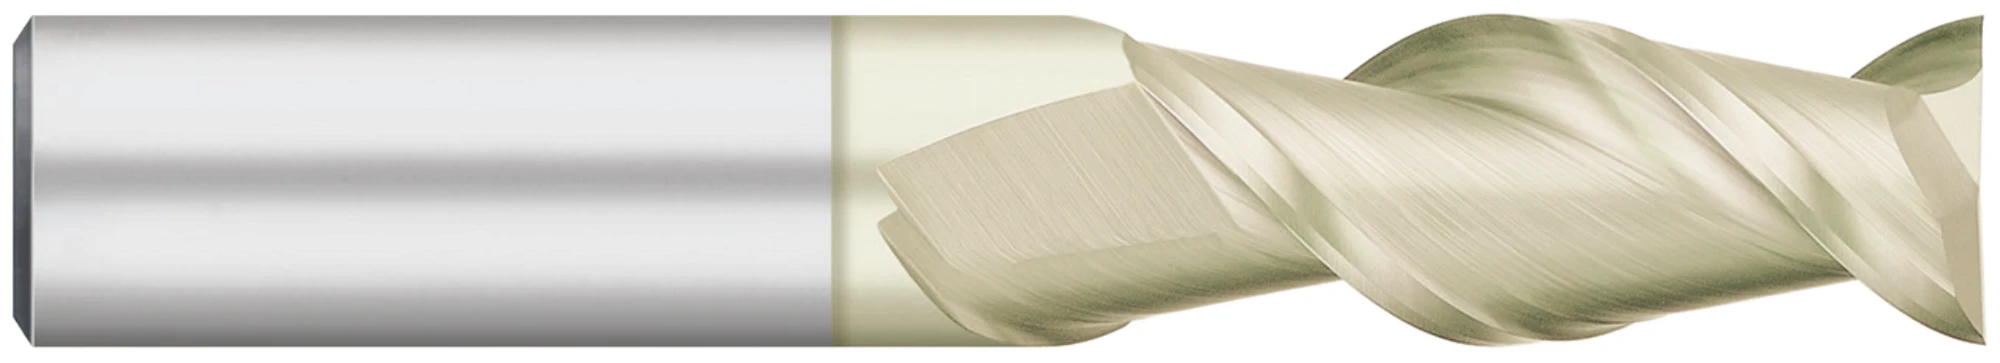
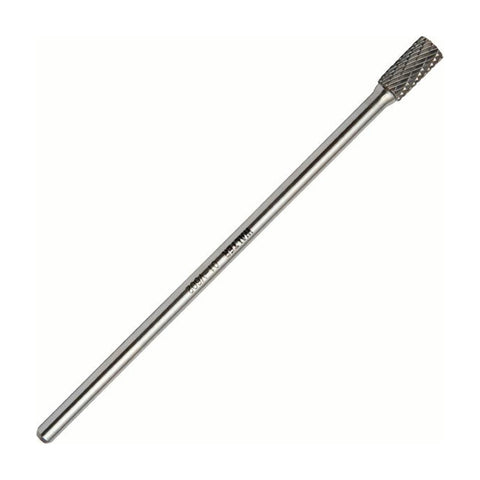
Every end mill in our end mills for aluminum collection ticks all four. They also cut brass, copper and other non-ferrous metals. If you are grinding aluminum by hand instead of milling it, the same chip problem applies to burrs; see carbide burrs for aluminum.
How to read an end mill label
An end mill label lists four sizes and two features, always in the same order. Take 3/8" x 1" x 2-1/2" .020r 3-Flute:
On the label |
What it means |
|---|---|
3/8" |
Cutting diameter. On every end mill we stock, the shank is the same size, so a 3/8 in. end mill needs a 3/8 in. collet or end mill holder. |
1" |
Length of cut (LOC): how deep the flutes reach. |
2-1/2" |
Overall length (OAL), tip to end of shank. |
.020r |
Corner radius, in inches. No "r" on the label means a square end. |
3-Flute |
Number of cutting edges. |
Square end mill or corner radius end mill: which should you buy?
Buy a square end mill only when the part needs a sharp 90° inside corner where the floor meets the wall. For everything else, buy a corner radius end mill. The sharp tip of a square end mill is the thinnest, hottest part of the tool, so it chips first. A small radius thickens that tip and spreads the load.
Trait |
Square end |
Corner radius |
|---|---|---|
Corner it leaves in the part |
Sharp 90° floor-to-wall |
Small fillet (.010, .020 or .040 in.) |
Tip strength |
Weakest point of the tool |
Stronger; chips less |
Tool life |
Shorter, ends at a chipped corner |
Longer |
Floor finish |
Can leave tool marks |
Smoother; the radius wipes the floor |
Part strength |
Sharp corner is a stress riser |
Fillet spreads load, good on brackets |
Mating parts |
Square bar or plate drops straight in |
Mating part needs a chamfer or clearance |
Price (same size) |
Base price |
Usually a few dollars more |
Pick a square end mill when a drawing calls for a sharp corner, or a square part has to sit flat in the pocket. Pick a corner radius end mill when the drawing allows any fillet, which on most fab-shop brackets, plates and fixtures it does.
Machinists also call a corner radius end mill a bull nose end mill. It is not a corner rounding end mill. A corner radius end mill is a normal end mill with rounded tips. A corner rounding end mill is a profile cutter that puts a round-over on the outside edge of a part. We stock the first kind, not the second.
2 flute or 3 flute end mill for aluminum?
Use a 3 flute end mill for most aluminum work and keep a 2 flute end mill for full-width slots and dry cutting. The extra flute gives a stiffer core, a better finish and a faster feed. The 2 flute gives the widest chip gap, which matters when the cutter is buried on both sides.
Job or setup |
Flutes |
Why |
|---|---|---|
Full-width slot or keyway |
2 |
Chips have nowhere to go but up the flute |
Cutting dry, no coolant or lube |
2 |
Most room before chips weld |
CNC router or a light hobby mill |
2 |
Lower cutting force |
Pockets, outside profiles, side milling |
3 |
Stiffer, faster feed, chips clear from the open side |
Manual knee mill with lube |
3 |
Better finish at hand-feed rates |
Finish pass on a wall or floor |
3 |
More edges per turn, smoother surface |
Four flutes and up belong on steel. On aluminum the gaps pack with chips in seconds. On our square end mills, flute count rarely changes the price: 2 and 3 flute cost the same in 22 of 27 sizes, so buy the flutes the job needs.
What length end mill do you need?
You need the shortest end mill that reaches the bottom of your deepest cut. Every extra inch of stick-out makes the tool bend more, chatter more and break sooner. We stock each diameter in three lengths:
Stub: length of cut about 1 to 2 times the diameter. Stiffest. Best for shallow pockets and finish passes.
Regular: about 2 to 3 times the diameter. The everyday length.
Long: about 3 to 6 times the diameter. For deep walls. Take lighter cuts.
On our corner radius end mills, the radius comes with the length. Up to 1/2 in., stub lengths carry a .010 in. radius, regular lengths .020 in. and long lengths .040 in. At 5/8 and 3/4 in., stubs are .020 in. and regular and long are .040 in. So if a drawing calls for a .040 in. fillet on a 1/4 in. end mill, the cutter is the long one.
Every end mill for aluminum we stock, by size
We stock 103 Titan USA carbide end mills for aluminum, from 1/8 to 1 in. in diameter. Each row below is one diameter and length. Prices are per end mill. A few small sizes have a 2- or 4-piece minimum, shown in brackets.
Diameter |
Length |
Length of cut |
Overall length |
Square, 2 flute |
Square, 3 flute |
Corner radius, 2 flute |
Corner radius, 3 flute |
|---|---|---|---|---|---|---|---|
1/8 in. |
Stub |
1/4 in. |
1-1/2 in. |
TC62100 $19.35 (min 2) |
TC63000 $19.35 (min 4) |
TC62400 .010 in. r, $26.57 (min 2) |
TC63600 .010 in. r, $23.85 (min 2) |
1/8 in. |
Regular |
1/2 in. |
1-1/2 in. |
TC62708 $27.05 (min 2) |
TC62908 $27.05 (min 2) |
TC64708 .020 in. r, $32.30 |
TC65908 .020 in. r, $32.30 (min 2) |
1/8 in. |
Long |
3/4 in. |
2-1/4 in. |
TC63308 $45.95 |
TC63508 $45.80 |
TC65308 .040 in. r, $54.75 |
TC66508 .040 in. r, $54.75 |
3/16 in. |
Stub |
3/8 in. |
2 in. |
TC62102 $28.80 (min 2) |
TC63002 $28.80 (min 2) |
TC62402 .010 in. r, $34.50 |
TC63602 .010 in. r, $34.50 (min 2) |
3/16 in. |
Regular |
5/8 in. |
2 in. |
TC62712 $37.50 (min 2) |
TC62912 $37.50 (min 2) |
TC64712 .020 in. r, $44.15 |
TC65912 .020 in. r, $44.15 |
3/16 in. |
Long |
3/4 in. |
2-1/2 in. |
TC63312 $52.75 |
TC63512 $52.75 |
TC65312 .040 in. r, $63.30 |
TC66512 .040 in. r, $63.30 |
1/4 in. |
Stub |
1/2 in. |
2 in. |
TC62104 $41.10 |
TC63004 $41.10 |
TC62404 .010 in. r, $48.50 |
TC63604 .010 in. r, $48.50 |
1/4 in. |
Regular |
3/4 in. |
2-1/2 in. |
TC62716 $52.45 |
TC62916 $52.45 |
TC64716 .020 in. r, $58.40 |
TC65916 .020 in. r, $58.40 |
1/4 in. |
Long |
1-1/4 in. |
3 in. |
TC63316 $71.85 |
TC63516 $71.85 |
TC65316 .040 in. r, $80.60 |
TC66516 .040 in. r, $80.60 |
5/16 in. |
Stub |
1/2 in. |
2 in. |
TC62106 $50.10 |
TC63006 $50.10 |
TC62406 .010 in. r, $45.05 |
TC63606 .010 in. r, $62.35 |
5/16 in. |
Regular |
13/16 in. |
2-1/2 in. |
TC62720 $62.20 |
TC62920 $62.20 |
TC64720 .020 in. r, $50.25 |
TC65920 .020 in. r, $69.45 |
5/16 in. |
Long |
1-3/8 in. |
3 in. |
TC63320 $97.75 |
TC63520 $97.75 |
TC65320 .040 in. r, $109.70 |
TC66520 .040 in. r, $109.70 |
3/8 in. |
Stub |
5/8 in. |
2 in. |
TC62108 $54.60 |
TC63008 $54.60 |
TC62408 .010 in. r, $66.85 |
TC63608 .010 in. r, $60.90 |
3/8 in. |
Regular |
1 in. |
2-1/2 in. |
TC62724 $65.85 |
TC62924 $65.85 |
TC64724 .020 in. r, $73.40 |
TC65924 .020 in. r, $73.40 |
3/8 in. |
Long |
1-1/2 in. |
4 in. |
TC63324 $117.05 |
TC63524 $117.05 |
TC65324 .040 in. r, $130.10 |
TC66524 .040 in. r, $130.10 |
1/2 in. |
Stub |
5/8 in. |
2-1/2 in. |
TC62110 $106.15 |
TC63010 $106.15 |
TC62410 .010 in. r, $113.20 |
TC63610 .010 in. r, $113.20 |
1/2 in. |
Regular |
1-1/4 in. |
3 in. |
TC62732 $119.95 |
TC62932 $119.95 |
TC64732 .020 in. r, $133.90 |
TC65932 .020 in. r, $133.90 |
1/2 in. |
Long |
2 in. |
4 in. |
TC63332 $189.85 |
TC63532 $189.85 |
TC65332 .040 in. r, $211.10 |
TC66532 .040 in. r, $211.10 |
5/8 in. |
Stub |
3/4 in. |
3 in. |
TC62112 $241.70 |
TC63012 $230.00 |
— |
TC63612 .020 in. r, $253.75 |
5/8 in. |
Regular |
1-5/8 in. |
3-1/2 in. |
TC62740 $257.90 |
TC62940 $257.90 |
TC64740 .040 in. r, $287.60 |
TC65940 .040 in. r, $275.40 |
5/8 in. |
Long |
2-3/8 in. |
5 in. |
TC63340 $440.40 |
TC63540 $440.40 |
TC65340 .040 in. r, $351.45 |
TC66540 .040 in. r, $470.30 |
3/4 in. |
Stub |
1 in. |
3 in. |
TC62114 $345.20 |
TC63014 $345.20 |
TC62414 .020 in. r, $269.90 |
TC63614 .020 in. r, $371.35 |
3/4 in. |
Regular |
1-3/4 in. |
4 in. |
TC62748 $370.40 |
TC62948 $370.40 |
TC64748 .040 in. r, $393.60 |
TC65948 .040 in. r, $393.60 |
3/4 in. |
Long |
2-1/2 in. |
5 in. |
TC63348 $478.25 |
TC63548 $478.25 |
TC65348 .040 in. r, $527.15 |
TC66548 .040 in. r, $510.70 |
1 in. |
Stub |
1-1/4 in. |
3-1/2 in. |
TC62116 $466.80 |
TC63016 $645.50 |
— |
— |
1 in. |
Regular |
1-3/4 in. |
4 in. |
TC62764 $648.05 |
TC62964 $651.05 |
— |
TC65964 .040 in. r, $520.10 |
1 in. |
Long |
2-1/4 in. |
5 in. |
TC63364 $825.50 |
TC63564 $800.25 |
— |
TC66564 .040 in. r, $638.85 |
Prices per end mill from our catalog, October 26, 2026. Shank diameter equals cutting diameter on every SKU. All are ZrN coated with a 45° helix.
Our picks for common fab-shop jobs
Job |
End mill |
Price |
Pick this when |
|---|---|---|---|
Pockets and outside profiles on brackets and plate |
TC65924 3/8 x 1 x 2-1/2 in., .020 in. radius, 3 flute |
$73.40 |
You want one end mill that does most aluminum work on a knee mill |
Full-width slots and keyways |
TC62724 3/8 x 1 x 2-1/2 in., square, 2 flute |
$65.85 |
The slot is the width of the cutter and needs square corners |
Square-bottom pocket for a mating part |
TC62924 3/8 x 1 x 2-1/2 in., square, 3 flute |
$65.85 |
A square bar or plate has to sit flat in the corner |
Deep walls, 1-1/2 in. and more |
TC66524 3/8 x 1-1/2 x 4 in., .040 in. radius, 3 flute |
$130.10 |
A regular length can't reach the floor |
Heavier stock removal, larger parts |
TC65932 1/2 x 1-1/4 x 3 in., .020 in. radius, 3 flute |
$133.90 |
Your mill has a 1/2 in. collet and the power for it |
CNC router or cutting dry |
TC64716 1/4 x 3/4 x 2-1/2 in., .020 in. radius, 2 flute |
$58.40 |
The machine is light or you can't run lube |
Small slots and detail |
TC62100 1/8 x 1/4 x 1-1/2 in., square, 2 flute |
$19.35 each, min 2 |
Features are under 1/4 in. wide |
Prices per end mill from our catalog, October 26, 2026.
How fast should you run a carbide end mill in aluminum?
Run a carbide end mill in aluminum as fast as your spindle allows, up to about 800 surface feet per minute as a starting point. The RPM formula is the same one in our drill speed chart: RPM = 3.82 × SFM ÷ diameter in inches.
Diameter |
Starting RPM at 800 SFM |
|---|---|
1/8 in. |
24,450 |
3/16 in. |
16,300 |
1/4 in. |
12,200 |
5/16 in. |
9,800 |
3/8 in. |
8,150 |
1/2 in. |
6,100 |
5/8 in. |
4,900 |
3/4 in. |
4,050 |
1 in. |
3,050 |
Most manual knee mills top out well below those numbers on anything under 5/8 in. That is fine. Run at the mill's top speed and keep the feed steady so the end mill cuts a real chip instead of rubbing. Rubbing is what heats aluminum and welds it to the flutes. Three habits help on any machine:
Lube or air. A mist, a brush of cutting fluid or WD-40, or a steady air blast to clear chips.
Ramp in. Enter the cut on a ramp or from the side instead of plunging straight down.
Climb mill on rigid machines. On a manual mill with backlash, conventional milling is safer.
Can you use an end mill without a milling machine?
You can use an end mill in a CNC router, but not in a drill press or a hand drill. A drill press is built for straight-down force. Side cutting loads the bearings sideways, can work the chuck off its taper and throws parts that are only held by hand.
A CNC router with a 1/4 in. or 1/2 in. collet runs our 1/4 and 1/2 in. end mills well in aluminum: use a 2 flute, take light passes and clamp the part hard. Without a mill or router, drill a row of holes and finish the edge with a file or an aluminum cut burr. For holes, see how to choose drill bits for metal.
Will these end mills cut steel?
No. Our end mills for aluminum are made for aluminum, brass, copper and other non-ferrous metals. Steel needs a different end mill: more flutes, a lower helix and a heat-resistant coating such as AlTiN. We don't sell a steel end mill online today. Call us if you need one.
From the shop floor
"Read an end mill label like a spec sheet, not a price tag: size, flutes, coating, profile. Those four details decide whether the tool cuts clean or burns out."
David Castro, President, Eldorado Tools
FAQ
What is the best end mill for aluminum?
The best end mill for aluminum is a solid carbide 2 or 3 flute end mill with a high helix and a ZrN or uncoated finish. For most fab-shop work, a 3/8 in. 3 flute corner radius end mill is the one to start with.
Can I use a 4 flute end mill on aluminum?
A 4 flute end mill will cut aluminum on a light finish pass, but it packs with chips on anything heavier. Use 2 or 3 flutes.
What does .020r mean on an end mill?
.020r means a corner radius of .020 in. on each cutting tip. No "r" on the label means a square end.
What is a bull nose end mill?
A bull nose end mill is another name for a corner radius end mill: a regular end mill with rounded tips that leaves a small fillet in the floor of a cut. It is different from a corner rounding end mill, which rounds over the outside edge of a part.
Why is aluminum sticking to my end mill?
Aluminum sticks when chips stay in the flutes and get recut. Use fewer flutes, raise the feed so the tool cuts instead of rubs, add lube or air, and avoid AlTiN coatings.
Are Titan end mills made in the USA?
Yes. Titan USA makes the end mills we stock in the United States.
Not sure which end mill fits your mill or your part? Call our team at (833) 4-ETOOLS or email sales@eldoradotools.com with the drawing or the job.
Sources: Titan USA product specifications (helix, coating, corner style, sizes); Eldorado Tools catalog prices, October 26, 2026; RPM formula as in our drill speed chart.
Change log: October 26, 2026, first draft.