


























































































































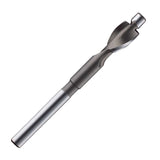
















End Mills Square End
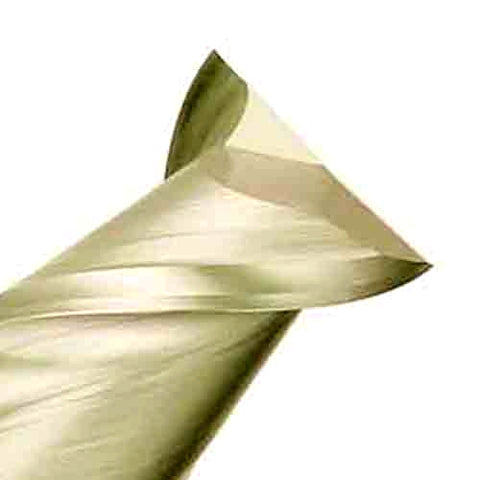
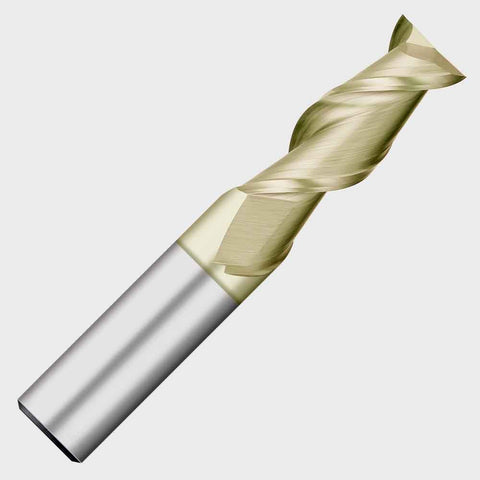
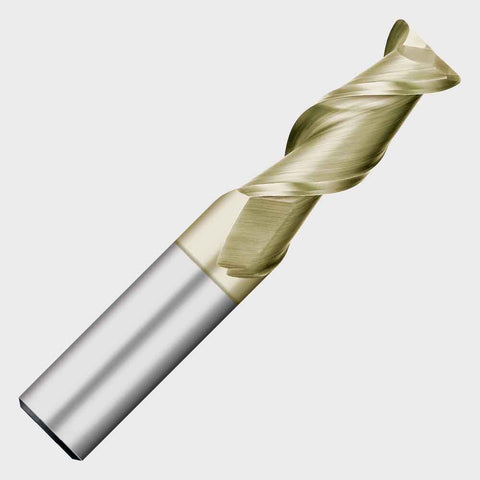
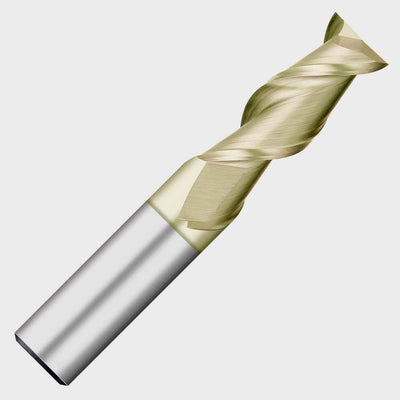
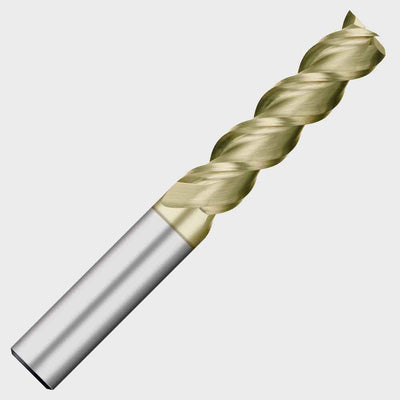
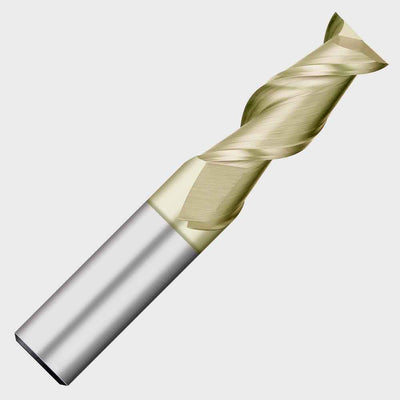
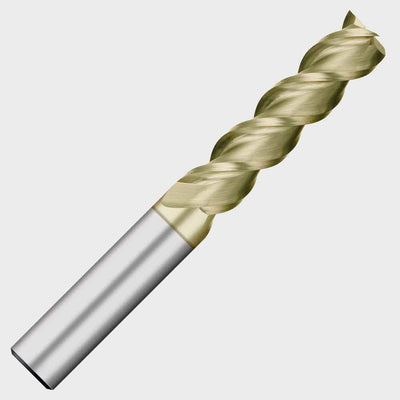
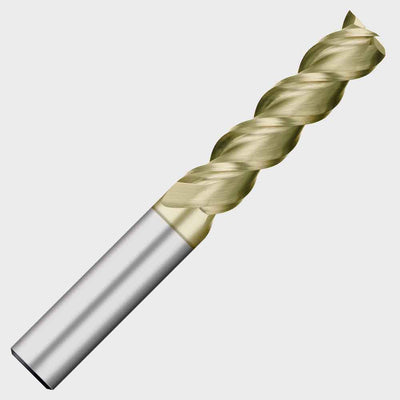
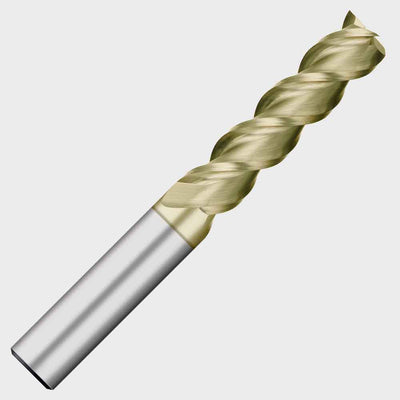
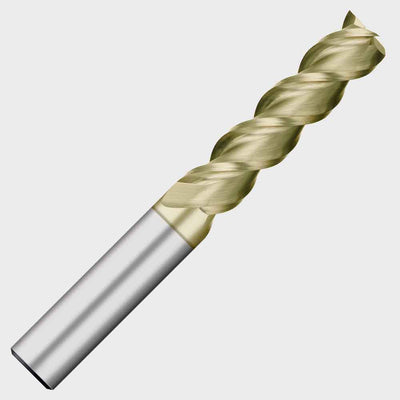
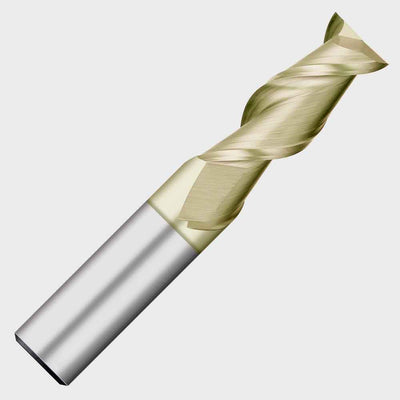
Titan squared carbide end mills for aluminum, in 2-flute and 3-flute styles from 1/8" to 1" diameter. For flat floors, slots, pockets and profiling.
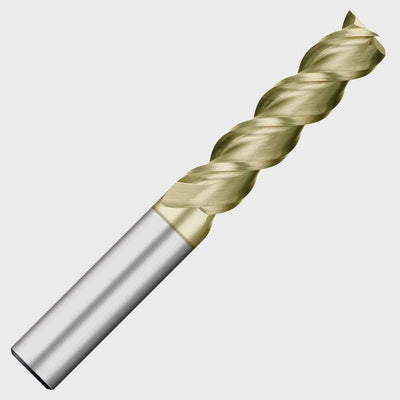

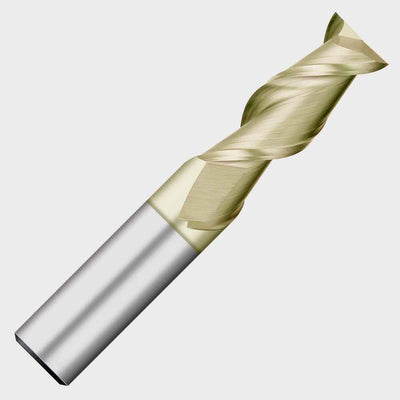
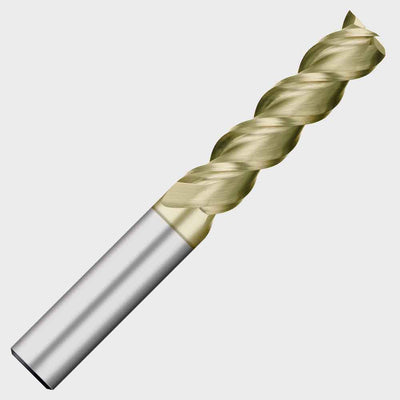
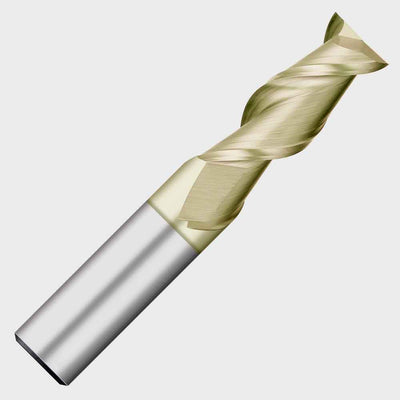
Choosing a square end mill
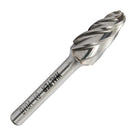
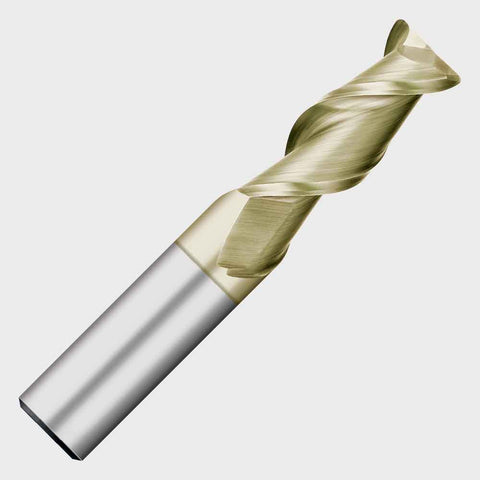
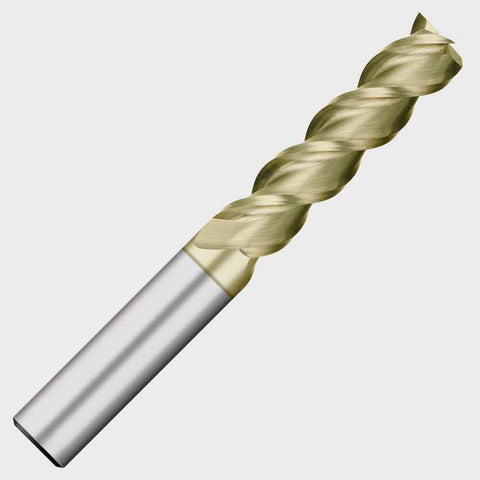
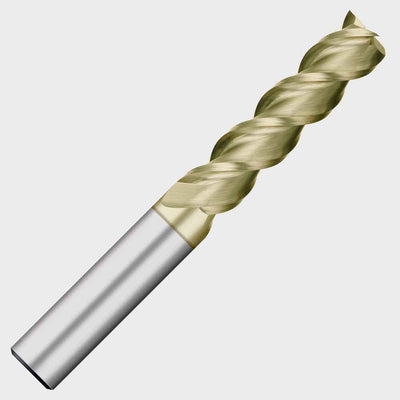
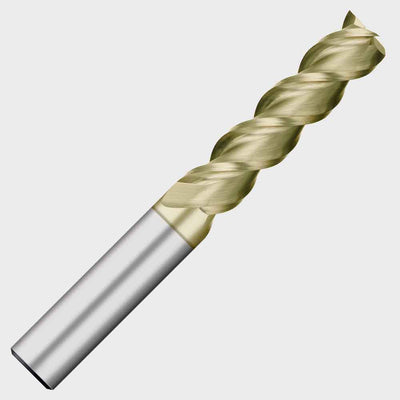
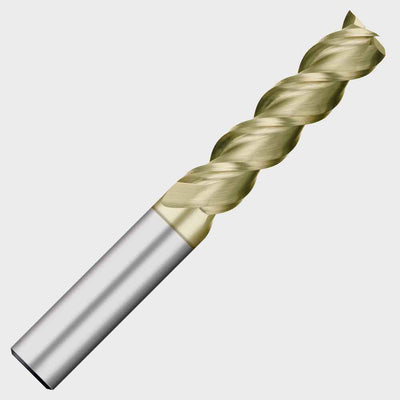
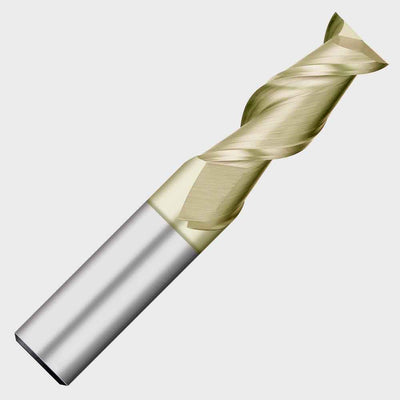
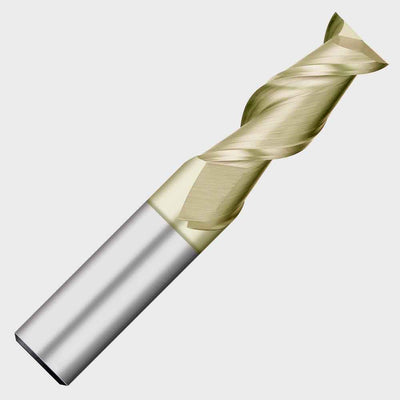
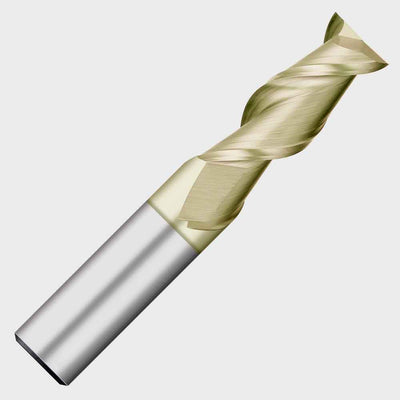
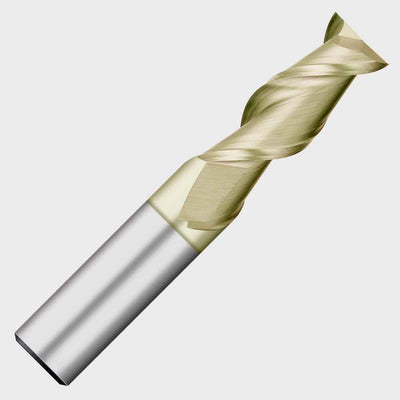
A square end mill has a flat bottom and sharp corners, so it leaves a flat floor and square inside corners. These 54 Titan squared carbide mills are made for aluminum and come in 2-flute and 3-flute versions, in diameters from 1/8" to 1".
Titles read diameter x length of cut x overall length. The same diameter comes in different reaches: 3/4" mills are listed as 1-3/4" x 4" and 2-1/2" x 5", for example. Pick the shortest length of cut that does the job, since short tools are stiffer.
Cutting tips
Aluminum wants high spindle speed and plenty of chip room. Use coolant or a cutting lubricant so chips do not weld to the flutes, clear chips as you go, and do not rub at too low a feed. Where a sharp corner is not required, a corner radius mill is stronger.
Free shipping on orders over $200. Trade accounts can reorder in a click from My Toolbox, or call (833) 438-6657.
Common questions
What do the three measurements in the title mean?
They read diameter x length of cut x overall length. A 1/2" x 2" x 4" mill is 1/2" across, with 2" of cutting flute and 4" overall.
Should I pick 2 flutes or 3?
Both are made for aluminum. Two flutes give more chip room in deep slots, and three flutes are stiffer. Use lubricant and clear chips either way.
Do I need coolant when milling aluminum?
Coolant or a cutting lubricant helps stop chips welding to the flutes, and it carries heat away. Clear chips as you go and keep the feed high enough that the mill is cutting, not rubbing.
Buying for a crew?
Call 833-438-6657, 8 AM to 4 PM MST. We know the parts, not just the part numbers.