






























































































































































HomeBlog & GuidesGuidesMetal Fabrication
Long Carbide Burrs and Mini Burrs for Pipe, Tanks and Ports
Long carbide burr or 1/8 in. mini? How deep each reaches into pipe, tanks and ports, the safe RPM for a 6 in. shank, and the exact Walter and Drillco picks.
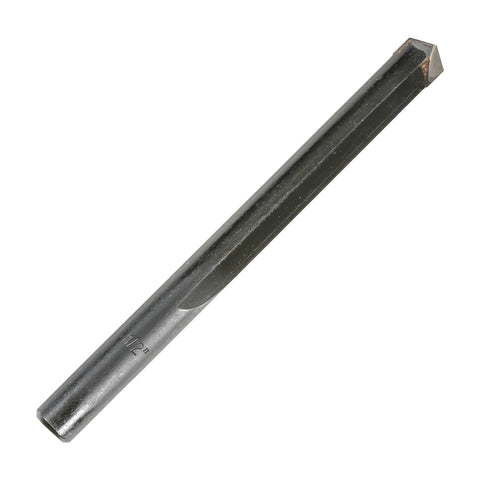
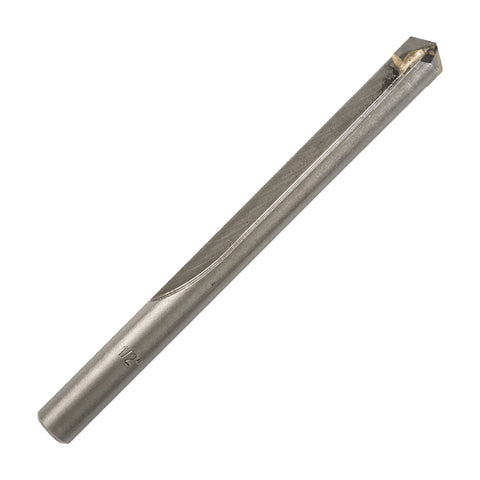
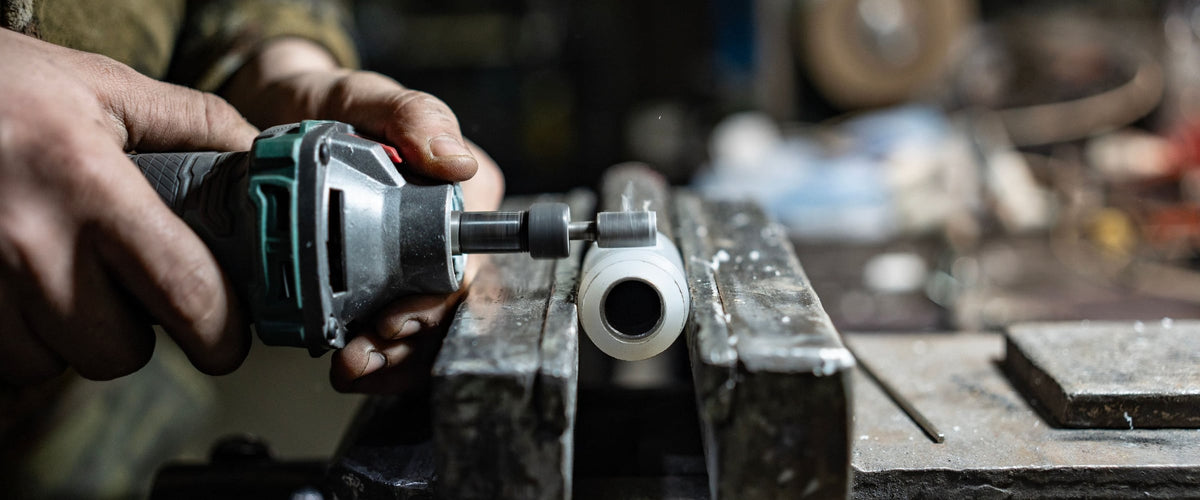
Quick answer: A long carbide burr puts a standard burr head on a 6 in. shank, so it reaches about 5 in. past the collet into pipe, tank nozzles and engine ports where the grinder body won't fit. Run it about 25% slower than the same head on a standard shank: roughly 8,250 to 16,500 RPM for a 1/2 in. head, by QTE North America's published speed chart. For openings under 3/8 in., use a miniature burr on a 1/8 in. shank. Walter's 6 in. burrs are $92.02 each. Drillco's 8-piece 1/8 in. set is $70.77.
Measure before you buy. You need two numbers: the size of the opening the burr goes through, and how far past that opening the work is. Then check which grinder you have. Those three facts pick the shank, the head size and the speed, and this guide goes through them in order of depth, from the lip of the opening inward.
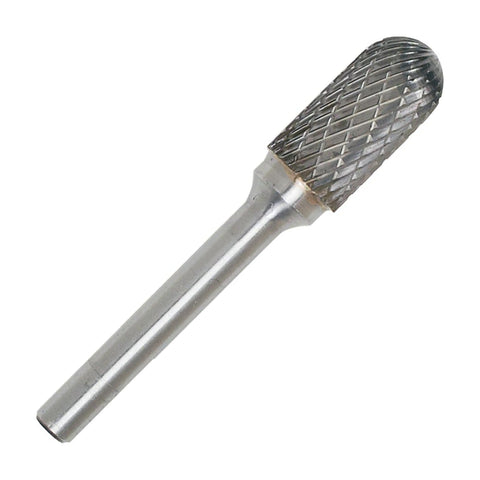
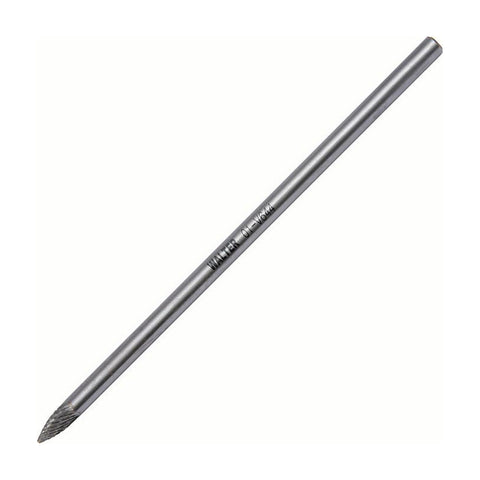
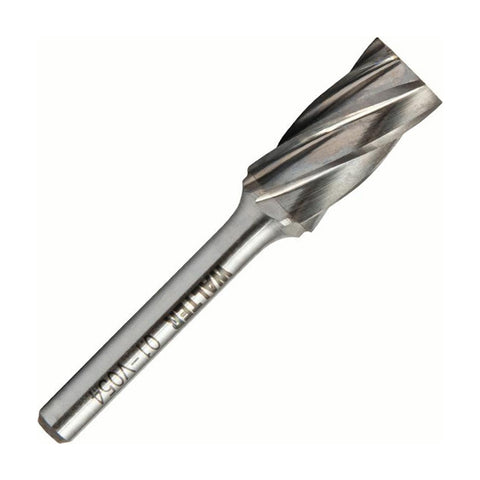
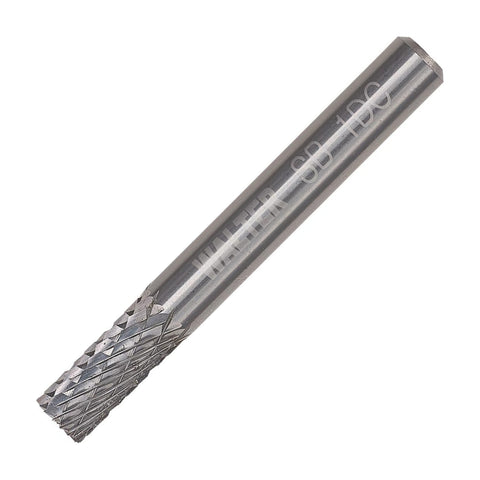
People call these long shank burrs, long reach burrs, extended shank burrs, L6 burrs, X-long burrs and long die grinder bits. The small ones are miniature burrs, 1/8 in. shank burrs, pencil grinder bits or Dremel burrs. A long burr is the same solid carbide head as a standard one, on a longer steel shank. A miniature burr is a smaller head on a thinner shank.
How deep can a long carbide burr reach?
A long carbide burr reaches about 5 in. past the grinder's collet, because about 1 in. of the 6 in. shank has to stay gripped. A standard 1/4 in. shank burr reaches about 1-1/4 in., and a miniature burr about 3/4 in. Past 5 in., no burr reaches safely.
The opening sets the head size. Leave about 1/8 in. of room around the head so you can steer it, which means a 1/2 in. head needs at least a 5/8 in. opening.
Burr |
Shank (in.) |
Reach past the collet (in.) |
Smallest opening (in.) |
|---|---|---|---|
Miniature |
1/8 |
3/4 |
1/4 |
Standard |
1/4 |
1-1/4 |
3/8 |
6 in. long |
1/4 |
5 |
3/8 |
Opening the burr goes through |
Depth past the opening |
What to use |
Example |
Price |
|---|---|---|---|---|
Under 1/4 in. |
Any |
Too small for any burr we stock |
A file, a deburring tool or a smaller tool |
— |
1/4 to 3/8 in. |
Up to 3/4 in. |
Miniature burr, 1/8 in. head, 1/8 in. shank |
01V021 SD-42 ball |
$23.60 each, min 2 |
1/4 to 3/8 in. |
Over 3/4 in. |
Not stocked |
We don't stock a longer 1/8 in. shank burr |
— |
3/8 in. and up |
Up to 1-1/4 in. |
Standard 1/4 in. shank burr |
01V001 SA-1 cylindrical |
$44.18 |
3/8 in. and up |
1-1/4 to 5 in. |
6 in. long burr |
01V601 SA-1 cylindrical, 6 in. |
$92.02 |
Wider than your grinder's nose |
Up to about 2-3/4 in. |
Standard burr; the grinder nose follows it in |
01V007 SC-5 |
$100.77 |
Any |
Over 5 in. |
No burr; use a flex shaft, or work from the other end |
— |
— |
Reach figures are typical for a properly seated burr and depend on your collet. Prices checked in our catalog on Nov 10, 2026.
"The long burr is the one we see come back bent. Someone chucks a 6 in. burr in a 22,000 RPM air grinder, pulls the trigger in open air, and the shank whips before it ever touches steel. Put the head on the work first, then run it slower than you'd run a short one."
David Castro, President, Eldorado Tools
Do you need a long burr at all?
You don't need a long burr when the work is within about an inch of the opening, or when the opening is wider than your grinder's nose, so the grinder can follow the burr in. A standard burr is stiffer, can run faster, and on some heads costs much less.
On six of the 17 heads the 6 in. burr costs exactly the same as the standard one, and on the SC-5 it costs $8.75 less. On the 1/4 in. heads the long shank adds up to $47.84. Here is every Walter long burr next to its standard twin.
Head |
Shape |
Head x cut length (in.) |
6 in. price |
Standard price |
6 in. SKU |
Standard SKU |
|---|---|---|---|---|---|---|
SA-1 |
Cylindrical |
1/4 x 5/8 |
$92.02 |
$44.18 |
||
SA-3 |
Cylindrical |
3/8 x 3/4 |
$92.02 |
$59.31 |
||
SA-5 |
Cylindrical |
1/2 x 1 |
$92.02 |
$88.95 |
||
SC-1 |
Cylindrical ball nose |
1/4 x 5/8 |
$92.02 |
$48.12 |
||
SC-3 |
Cylindrical ball nose |
3/8 x 3/4 |
$92.02 |
$65.35 |
||
SC-5 |
Cylindrical ball nose |
1/2 x 1 |
$92.02 |
$100.77 |
||
SD-1 |
Ball |
1/4 x 7/32 |
$92.02 |
$47.22 |
||
SD-3 |
Ball |
3/8 x 5/16 |
$92.02 |
$48.12 |
||
SD-5 |
Ball |
1/2 x 7/16 |
$92.02 |
$66.11 |
||
SF-1 |
Round nose tree |
1/4 x 5/8 |
$92.02 |
$92.02 |
||
SF-3 |
Round nose tree |
3/8 x 3/4 |
$92.02 |
$62.18 |
||
SF-5 |
Round nose tree |
1/2 x 1 |
$92.02 |
$92.02 |
||
SG-1 |
Pointed tree |
1/4 x 5/8 |
$92.02 |
$92.02 |
||
SG-3 |
Pointed tree |
3/8 x 3/4 |
$92.02 |
$92.02 |
||
SG-5 |
Pointed tree |
1/2 x 1 |
$92.02 |
$92.02 |
||
SL-3 |
Cone, 14° |
3/8 x 1-1/16 |
$92.02 |
$73.22 |
||
SL-5 |
Cone, 14° |
5/8 |
$92.02 |
$92.02 |
All Walter 01V, double cut, 1/4 in. shank, sold each. Prices checked in our catalog on Nov 10, 2026.
Every long burr's maximum speed is half the standard one (see the speed table below). That is the cost of reach: a 6 in. shank flexes, so it can't spin as fast. For head shapes and codes, see the carbide burr shapes chart.
What is the best carbide burr for grinding inside a pipe?
The best carbide burr for grinding inside a pipe is a 6 in. double cut cylindrical ball nose burr (SC), because the rounded end can't dig a corner into the curved wall. Use a round nose tree (SF) for a nozzle or tapping, a ball (SD) for a pocket, and a pointed tree (SG) for a tight corner.
Job |
Head |
SKU |
Size |
Price |
Why this one |
|---|---|---|---|---|---|
Weld root or icicles inside pipe, 2 to 5 in. from the end |
Cylindrical ball nose |
SC-5, 1/2 x 1 in., 6 in. long |
$92.02 |
Flattens the root without cutting a corner into the wall. Costs less than the standard SC-5. |
|
Smaller pipe or tube, 3/4 to 1-1/4 in. inside |
Cylindrical ball nose |
SC-3, 3/8 x 3/4 in., 6 in. long |
$92.02 |
Leaves room to steer inside the bore. |
|
Tank nozzle, manway lip or fitting bore |
Round nose tree |
SF-5, 1/2 x 1 in., 6 in. long |
$92.02 |
Follows the bore and blends the weld where the nozzle meets the shell. Same price as standard. |
|
Pocket or bowl at the bottom of a port |
Ball |
SD-3, 3/8 in., 6 in. long |
$92.02 |
A ball reaches a curved floor. |
|
Tight corner or slot deep in a weldment |
Pointed tree |
SG-3, 3/8 x 3/4 in., 6 in. long |
$92.02 |
The point gets into the corner. Same price as standard. |
|
Cast iron hub or straight fitting bore |
Cylindrical |
SA-5, 1/2 x 1 in., 6 in. long |
$92.02 |
Cleans a straight bore. Only $3.07 more than standard. |
All of these are double cut, the right cut for steel, stainless and cast iron. Walter also rates them for brass and bronze. Aluminum loads up a double cut burr. We stock aluminum cut burrs only in standard length, so for aluminum heads and manifolds read carbide burrs for aluminum first.
After the burr, blend the surface with a mounted point on the same grinder. Walter's 12D723 W-205 is 3/4 x 1 in. on a 1/4 in. shank, made for stainless, at $4.71 each (minimum 10). Check the point's RPM rating before you run it.
What RPM should a 6 in. long carbide burr run at?
Run a 6 in. long carbide burr about 25% slower than the same head on a standard shank. QTE North America's carbide burr speed chart says extra long burrs "should be run 25% slower than a standard burr." QTE's chart gives a 1/2 in. head 11,000 to 22,000 RPM on a standard shank, so a 6 in. burr with that head runs about 8,250 to 16,500 RPM. Walter rates its 1/2 in. long burrs to 25,000 RPM at most. The table puts the two published sources side by side, with Walter's maximums.
Head diameter (in.) |
Standard shank, RPM (QTE chart) |
6 in. long, RPM (QTE) |
Drillco rule, RPM (1,500 to 3,000 SFM) |
Walter max, 6 in. |
Walter max, standard |
|---|---|---|---|---|---|
1/8 (miniature) |
45,000 to 90,000 |
No long version stocked |
45,800 to 91,700 |
— |
Not listed |
1/4 |
23,000 to 45,000 |
17,000 to 33,000 |
22,900 to 45,800 |
35,000 |
70,000 |
3/8 |
15,000 to 30,000 |
11,250 to 22,500 |
15,300 to 30,600 |
33,000 |
66,000 |
1/2 |
11,000 to 22,000 |
8,250 to 16,500 |
11,500 to 22,900 |
25,000 |
50,000 |
5/8 |
Not on QTE's chart: use Drillco's 9,200 to 18,300 |
Not on QTE's chart: use 6,900 to 13,800 |
9,200 to 18,300 |
20,000 |
40,000 |
QTE columns: QTE North America, "Speeds & Feeds for Carbide Burrs." QTE prints the 1/4 x 6 in. figure itself; the other 6 in. figures are its standard range less 25%, per its rule that "extra long carbide burrs should be run 25% slower than a standard burr." Drillco column: Drillco Magnum Solid Carbide Burs catalog, p. 15, working speed 1,500 to 3,000 surface feet per minute, as RPM (SFM x 3.82 / diameter, nearest 100). Maximums: Walter product data.
The two published sources agree within a few hundred RPM. Where they differ, staying inside both is the safe choice. These are working ranges, not ratings: never run a burr above its own maximum or the grinder's. Inside a range, Drillco says lower speeds remove material faster and higher speeds leave a better finish.
A fixed-speed air die grinder is often rated at 20,000 RPM or more, which is above the working range for a 1/2 in. long burr. Feather the throttle, fit an inline regulator, or use a variable-speed grinder. Walter's 30A141 DIALSPEED 6141 point grinder ($579.42) dials from 10,000 to 30,500 RPM, which covers every long-burr range in the table. It has a 1/4 in. collet.
Three habits keep a long burr straight. Put the head against the work before you pull the trigger, never in open air. Seat as much shank in the collet as the job allows. Let the teeth cut, with light pressure.
Which carbide burr fits a Dremel or pencil grinder?
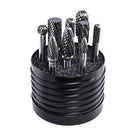
A Dremel, a rotary tool or a pencil grinder takes a miniature burr on a 1/8 in. shank. Start with a set: Drillco's 8-piece No. 6 set (70S006DC) has eight 1/8 in. heads for $70.77, or $8.85 a burr, made in the USA. The cheapest order of Walter miniatures is two burrs at $23.60 each.
Head |
Shape |
Head x cut length (in.) |
Price |
Sold |
SKU |
|---|---|---|---|---|---|
SA-43 |
Cylindrical |
1/8 x 9/16 |
$23.60 |
Each, min 2 |
|
SD-42 |
Ball |
1/8 x 1/8 |
$23.60 |
Each, min 2 |
|
SF-42 |
Round nose tree |
1/8 x 1/2 |
$23.60 |
Each, min 2 |
|
SG-44 |
Pointed tree |
1/8 x 1/2 |
$23.60 |
Each, min 2 |
|
SL-42 |
Cone, 14° |
1/8 x 1/2 |
$23.60 |
Each, min 2 |
|
SM-42 |
Conical |
1/8 x 7/16 |
$23.60 |
Each, min 2 |
|
Drillco No. 6 set, 8 pieces |
SA, SC, SD, SE, SF, SG, SL, SN |
1/8 heads |
$70.77 |
Set, $8.85 a burr |
|
Drillco No. 7 set, 8 pieces |
SA, SB, SC, SD, SE, SF, SG, SM |
1/4 heads on 1/8 shank |
$131.45 |
Set, $16.43 a burr |
Walter miniatures are double cut, made in China. Drillco sets come in double cut (DC) or single cut (SC) at the same price. Prices checked in our catalog on Nov 10, 2026.
Miniatures are for cross-drilled holes in hydraulic manifolds, small dies, tapped holes, lettering and the inside of small fittings. QTE's chart gives a 1/8 in. head 45,000 to 90,000 RPM, and its notes add that burrs up to 1/8 in. "may be run at speeds up to 75,000 RPM, depending on the material being cut and amount of shank exposed." Most rotary tools top out near 35,000 RPM, which is below the working range, so the burr cuts more slowly. Keep the pressure light; a 1/8 in. shank snaps if you lean on it.
The DIALSPEED takes 1/4 in. shanks only, so it won't hold these. For blending after a miniature, Walter's 12D232 B-52 mounted point is 3/8 x 3/4 in. on a 1/8 in. shank, $3.65 each (minimum 10). For the Dremel question in more detail, see carbide burr shapes.
Why does my long burr wobble or bend?
A long burr wobbles because it is spinning too fast for its length. Check speed first, then the collet, how much shank is gripped, and how hard you are pushing.
What you see |
Likely cause |
What to do |
|---|---|---|
Shank whips as soon as you pull the trigger |
Started in open air, or speed too high |
Put the head on the work first. Slow down to the range in the speed table. |
Wobble that gets worse the deeper you go |
Too little shank in the collet |
Seat more shank. If the job needs all 6 in., slow down further. |
Burr grabs and climbs the wall |
Too much side pressure, or a pointed head on a curved wall |
Lighten up. Change to a ball nose (SC) or round nose (SF). |
Chatter even at low speed |
Worn or dirty collet |
Blow out the collet and spindle. Replace a scored collet. |
Shank is visibly bent |
Overspeed or side load |
Throw it away. Don't straighten it; a bent shank can snap the head off. |
Head chipped |
Dropped, or forced into hard metal |
Replace it. For hardened steel, use a hard alloy burr such as the SF-5 01V034 (standard length only). |
Head packed silver and smooth |
Aluminum loaded the double cut teeth |
Use an aluminum cut burr. We stock those in standard length. |
What to check before grinding inside a tank
Before grinding inside a tank, find out what it held, whether it counts as a permit-required confined space under OSHA's rules (29 CFR 1910.146 in general industry), and whether your site needs a hot-work permit. Grinding sparks inside a vessel that held fuel or solvent can ignite what's left. Ventilate, wear a face shield over safety glasses, and use hearing protection, because a tank amplifies the noise.
Is a $92 long burr worth it next to a cheap set?
A $92 long burr is worth it if you run it in steel or stainless every week. At 5 in. from the collet, balance and the joint between head and shank matter more than on a standard burr, and that is where cheap long burrs fail. If you need one once a year in mild steel, a budget set will do the job.
Buy only the heads your work uses. For pipe welds that is usually one SC and one SF. In the 1/2 in. size both cost no more in the long version: the SC-5 is $8.75 less and the SF-5 is the same price. So are the SF-1, all three pointed trees and the SL-5.
Here is what to buy for each job, starting with one burr or the full kit.
Job |
Trade |
Start with |
Full kit |
After the burr |
|---|---|---|---|---|
Pipe weld root |
Metal fab |
01V607 SC-5 cylindrical ball nose, 6 in., $92.02 |
01V607 SC-5, 6 in., $92.02; 01V606 SC-3 for smaller bores, 6 in., $92.02; 12D723 W-205 mounted point for stainless, 10 x $4.71 |
Flap disc for the cap outside |
Tank nozzle and shell |
Fab, plumbing |
01V615 SF-5 round nose tree, 6 in., $92.02 |
01V615 SF-5, 6 in., $92.02; 01V626 SD-5 ball, 6 in., $92.02; DB-18 deburring tool, 5 x $17.74 |
Step drill for a bigger hole in a thin wall |
Hubs, fittings and pipe ends |
Plumbing |
01V605 SC-1 cylindrical ball nose, 6 in., $92.02; RIM-01 inner rim reamer, 2 x $20.75 |
01V605 SC-1, 6 in., $92.02; 01V604 SA-5 cylindrical, 6 in., $92.02; RIM-02 inner rim reamer, 2 x $29.52 |
Reamer for cut pipe ends |
Ports and runners |
Automotive |
01V641 SF-1 round nose tree, 6 in., $92.02 |
01V641 SF-1, 6 in., $92.02; 01V610 SD-3 ball, 6 in., $92.02; 01V606 SC-3, 6 in., $92.02 |
Aluminum cut for aluminum heads |
Cross-drilled holes |
Hydraulics, die work |
01V021 SD-42 ball, 1/8 in., 2 x $23.60 |
70S006DC Drillco No. 6, 8 heads, $70.77; 01V021 spare SD-42 balls, 2 x $23.60 |
Deburring tool for the hole edge |
Rotary tool owners |
Knife, jewelry, hobby |
70S006DC Drillco No. 6, 8 heads, 1/8 in., $70.77 |
70S006DC Drillco No. 6, $70.77; 70S007DC Drillco No. 7, 1/4 in. heads on 1/8 in. shank, $131.45 |
12D232 B-52 mounted point on a 1/8 in. shank to blend, $3.65 each, box of 10 |
Prices checked in our catalog on Nov 10, 2026. Mounted points, deburring tools and reamers are sold with a minimum.
What else do you need with a long carbide burr?
A long carbide burr does the heavy cutting. The tools below finish the job, and each one fits a different tool. Check the Fits column before you order: the reamers and the deburring tool do not go in a die grinder.
Accompanying bits and what each one fits
Bit |
What it does next to the burr |
Shank |
Fits |
Price |
Read |
|---|---|---|---|---|---|
12D723 W-205 mounted point, 3/4 x 1 in., for stainless |
Blends a weld root after the burr |
1/4 in. round |
Die grinder or DIALSPEED, up to 34,500 RPM |
$4.71 each, box of 10 |
— |
12D593 W-179 mounted point, 3/8 x 1-1/4 in., for stainless |
Blends inside smaller pipe and tube |
1/4 in. round |
Die grinder or DIALSPEED, up to 45,750 RPM |
$5.69 each, box of 10 |
— |
12D232 B-52 mounted point, 3/8 x 3/4 in., for mild steel |
Blends after a miniature burr |
1/8 in. round |
Rotary tool or pencil grinder, up to 45,370 RPM |
$3.65 each, box of 10 |
— |
RIM-01 inner rim reamer, 1/8 to 3/4 in. |
Cleans the inside edge of a cut pipe end |
1/4 in. impact hex |
Drill or impact driver. Not a die grinder. |
$20.75 each, min 2 |
|
RIM-02 inner rim reamer, 3/16 to 7/8 in. |
Same, for larger tube |
1/4 in. impact hex |
Drill or impact driver. Not a die grinder. |
$29.52 each, min 2 |
|
DB-18 90° deburring tool, 3/16 to 17/32 in. holes |
Cleans a drilled hole edge in plate or a tank wall |
1/4 in. round |
Drill. Not a die grinder. |
$17.74 each, min 5 |
|
30A141 Walter DIALSPEED 6141 point grinder |
Runs the long and standard burrs at the right speed |
Takes 1/4 in. shanks only |
10,000 to 30,500 RPM |
$579.42 |
— |
Maximum speeds from Walter's product data. Prices checked in our catalog on Nov 10, 2026.
For the rest of the job: cut the pipe first with a cut-off wheel, finish the weld cap outside with a flap disc, enlarge a round hole in a thin wall with a step drill, and clean stainless with a stainless wire cup brush.
FAQ
Should I use a die grinder extension or a long burr?
A long burr is simpler and stiffer, because there is one joint instead of two. An extension makes sense when you need a head size or shape we don't stock in 6 in. Either way, run 25% slower than a standard burr.
Can I cut a long burr shorter?
No. Cutting the shank leaves a rough end that won't seat true in the collet, and the burr will run out. Buy the length you need.
Can I straighten a bent burr shank?
No. A bent shank has already been overloaded and can snap at speed. Throw it away.
Will a 6 in. burr fit my Dremel?
No. Our long burrs have a 1/4 in. shank, and a Dremel takes 1/8 in. Use a miniature burr instead.
What size collet does a pencil grinder use?
Most pencil grinders take a 1/8 in. or 3 mm collet, and some take 1/4 in. Check the nameplate, then match the burr's shank to it exactly.
Can I use a long burr to port an aluminum cylinder head?
Not ours. Our long burrs are double cut, which loads up on aluminum. Read carbide burrs for aluminum for the right cut, and use a standard-length aluminum cut burr where it reaches.
Will these burrs cut copper and brass fittings?
Walter rates these burrs for brass and bronze. Copper isn't on the list. If you use one on copper, take light passes and clear the teeth often.
How long do carbide burrs last?
No fixed number holds, because metal, speed and pressure all change it. A burr is done when it stops throwing chips and starts making heat.
Do you have a long burr for hardened steel?
Not yet. Our hard alloy burrs, such as the SF-5 01V034, are standard length.
Not sure which length or head fits the job? Call our team at (833) 4-ETOOLS or email sales@eldoradotools.com with the opening size, the depth and your grinder, and we will name the burr.
Related: the full 6 in. long shank burr range, miniature burrs, carbide burr sets and point grinders.
Sources: Walter product specifications; Drillco Magnum Solid Carbide Burs catalog, p. 15; QTE North America, Speeds & Feeds for Carbide Burrs; OSHA 29 CFR 1910.146.
First published [date], with prices checked in our catalog on Nov 10, 2026.