





















































HomeBlog & GuidesGuidesMetal Fabrication
Drill Speed Chart: The Right RPM, and Why Heat Kills Bits
Starting RPM for drill bits, hole saws, step drills and countersinks in aluminum, brass, steel, cast iron and stainless, plus how to stop overheating.
Quick answer: Every drill speed chart follows one rule: drill metal slower as the bit gets bigger and the metal gets harder. Starting speed in RPM = 3.82 × cutting speed (SFM) ÷ bit diameter in inches. For a high-speed steel (HSS) bit, that works out to about 1,400 RPM for a 1/4 in. bit in mild steel, 600 RPM in stainless and 3,800 RPM in aluminum. A 2 in. bi-metal hole saw in mild steel wants only about 150 RPM. Set a step drill for its biggest step. If the chips turn blue or the tool squeals, it is too hot: slow down, push harder and add cutting oil.
What RPM should I drill metal at?
The right drill speed for metal depends on two things: the metal and the bit diameter. Harder metal and bigger bits both need a slower speed. This drill speed chart gives starting RPMs for HSS twist drill bits. Cobalt bits start at the same speeds.
| Bit size | Aluminum | Brass | Mild steel | Cast iron | Stainless steel |
|---|---|---|---|---|---|
| 1/16 in. | 15,300 | 9,150 | 5,500 | 4,300 | 2,450 |
| 1/8 in. | 7,650 | 4,600 | 2,750 | 2,150 | 1,200 |
| 3/16 in. | 5,100 | 3,050 | 1,850 | 1,450 | 800 |
| 1/4 in. | 3,800 | 2,300 | 1,400 | 1,050 | 600 |
| 5/16 in. | 3,050 | 1,850 | 1,100 | 850 | 500 |
| 3/8 in. | 2,550 | 1,550 | 900 | 700 | 400 |
| 7/16 in. | 2,200 | 1,300 | 800 | 600 | 350 |
| 1/2 in. | 1,900 | 1,150 | 700 | 550 | 300 |
| 5/8 in. | 1,550 | 900 | 550 | 450 | 240 |
| 3/4 in. | 1,250 | 750 | 450 | 350 | 200 |
| 1 in. | 950 | 550 | 350 | 270 | 150 |
RPM for HSS and cobalt twist drills. Starting cutting speeds: aluminum 250, brass 150, mild steel 90, cast iron 70 and stainless steel 40 surface feet per minute (SFM). Rounded to the nearest 50 RPM, or 10 below 300.
Treat every number as a place to start, not a rule. A sharp bit in a drill press with cutting oil can go a little faster. A hand drill, a long bit, a dull bit or a dry cut should go a little slower. Stainless steel needs a cobalt bit, not plain HSS.
How do I calculate drill RPM?
To calculate drill RPM, multiply the cutting speed in surface feet per minute (SFM) by 3.82, then divide by the tool diameter in inches: RPM = 3.82 × SFM ÷ D. The 3.82 is 12 ÷ π. It turns feet per minute at the cutting edge into turns per minute of the spindle.
Example: a 1/2 in. HSS bit in mild steel. 3.82 × 90 SFM ÷ 0.5 in. = 688 RPM, so start at about 700 RPM. The same bit in stainless: 3.82 × 40 ÷ 0.5 = 306, so about 300 RPM.
In metric, RPM = cutting speed (m/min) × 1,000 ÷ (π × diameter in mm). 90 SFM is about 27 m/min.
| Tool | Aluminum | Brass | Mild steel | Cast iron | Stainless steel |
|---|---|---|---|---|---|
| HSS or cobalt twist drill, HSS step drill | 250 | 150 | 90 | 70 | 40 |
| Carbide-tipped drill (drill press only) | 500 | 300 | 180 | 140 | 80 |
| Bi-metal hole saw | 190 | 130 | 80 | 60 | 40 |
| HSS countersink | 125 | 75 | 45 | 35 | 20 |
Starting cutting speeds in SFM that we use for every speed on this page.
Why the speed has to drop as the tool grows: the outside edge of a bigger tool travels farther on every turn. A 2 in. hole saw at 700 RPM moves its teeth about four times faster than a 1/2 in. bit at 700 RPM. That extra speed at the edge is extra heat.
What speed should I run a hole saw in metal?
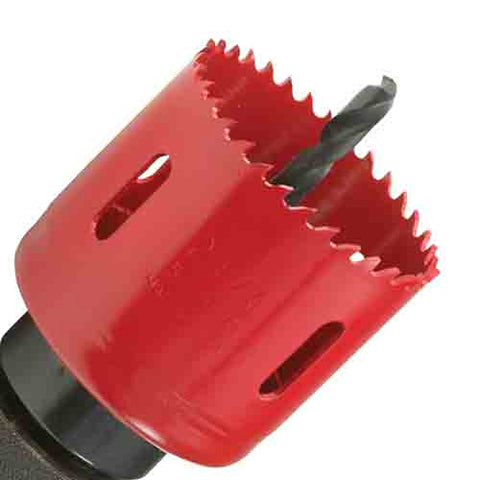
Run a hole saw in metal much slower than a drill bit: about 150 RPM for a 2 in. bi-metal hole saw in mild steel, and about 80 RPM in stainless. The teeth are on the outside of a large circle, so they move fast even at a low RPM.
| Hole saw size | Aluminum | Brass | Mild steel | Cast iron | Stainless steel |
|---|---|---|---|---|---|
| 3/4 in. | 950 | 650 | 400 | 300 | 200 |
| 7/8 in. | 850 | 550 | 350 | 260 | 170 |
| 1 in. | 750 | 500 | 300 | 230 | 150 |
| 1-1/8 in. | 650 | 450 | 270 | 200 | 140 |
| 1-3/8 in. | 550 | 350 | 220 | 170 | 110 |
| 1-1/2 in. | 500 | 350 | 200 | 150 | 100 |
| 2 in. | 350 | 250 | 150 | 110 | 80 |
| 2-1/2 in. | 290 | 200 | 120 | 90 | 60 |
| 3 in. | 240 | 170 | 100 | 80 | 50 |
| 4 in. | 180 | 120 | 80 | 60 | 40 |
RPM for bi-metal hole saws. Starting cutting speeds: aluminum 190, brass 130, mild steel 80, cast iron 60 and stainless 40 SFM.
A bi-metal hole saw is the one to use in steel. Our hole saws include ITM bi-metal variable-pitch saws, made in the USA with M3 high-speed steel teeth. The 2 in. ITM bi-metal hole saw (275HW0028) is $12.24 each (min. 4), and the 7/8 in. (275HW0016) for conduit knockouts is $7.94 each (min. 4). ITM's carbide-tipped hole saws are made for wood, fiberglass, laminate and cast iron, not sheet steel.
Use cutting oil on steel and stainless, and add more on every hole.
Keep the saw flat. Rocking it breaks teeth and makes an oval hole.
Back out and clear chips in plate thicker than about 1/4 in.
Ease off at breakthrough. The saw grabs as it exits thin metal.
What speed should I use for a step drill bit?
Set a step drill bit for the largest step you will cut, then leave it there. The biggest step is the part that runs hottest. A step drill that ends at 7/8 in. wants about 400 RPM in mild steel, even though its 1/8 in. tip could spin much faster.
| Largest step you will cut | Aluminum | Mild steel | Stainless (cobalt step drill) |
|---|---|---|---|
| 1/2 in. | 1,900 | 700 | 300 |
| 3/4 in. | 1,250 | 450 | 200 |
| 7/8 in. | 1,100 | 400 | 170 |
| 1-1/8 in. | 850 | 300 | 140 |
| 1-3/8 in. | 700 | 250 | 110 |
Step drill RPM, using the same starting cutting speeds as an HSS twist drill.
Step drills are made for sheet metal up to about 1/8 in. thick: electrical boxes, panels, studs, duct and auto body. The ITM M2 step drill, 1/8–1/2 in. (274HEX01) is $32.86 each (min. 2), with a 1/4 in. hex shank for impact drivers. For stainless steel, use the M35 cobalt step drill with TiAlN coating (XSTP-01) at $37.96. See every size in our step drill collection.
What speed should I run a countersink?
Run a countersink at about half the speed of a drill bit the same size. A countersink cuts with its whole cone at once, so too much speed makes it chatter and leave a rough, many-sided hole. For a 3/4 in. countersink in mild steel, start near 230 RPM.
| Countersink body diameter | Aluminum | Mild steel | Stainless steel |
|---|---|---|---|
| 1/2 in. | 950 | 350 | 150 |
| 3/4 in. | 650 | 230 | 100 |
| 1 in. | 500 | 170 | 80 |
If it chatters, slow down and push a little harder. Our countersinks include Weldon 82° pointless (single-flute) countersinks, which are built to cut without chatter. The CS-18 (3/16 to 17/32 in.) is $18.04 each (min. 10).
How do I set the speed on a cordless drill or drill press?
On a cordless drill, pick the gear first and then use the trigger. Most two-speed cordless drills run up to about 450–600 RPM in low gear (1) and 1,500–2,000 RPM in high gear (2). On a drill press, pick the belt step closest to, but below, the chart number.
| Target RPM | Cordless drill | Examples |
|---|---|---|
| Under 300 | Low gear, trigger about half way or less | 2 in. hole saw in steel, 1/2 in. bit in stainless |
| 300 to 550 | Low gear, trigger most of the way | 7/8 in. step drill in steel, 3/8 in. bit in stainless |
| 550 to 1,800 | High gear, part trigger | 1/4 in. bit in mild steel, 1/2 in. bit in aluminum |
| Over 1,800 | High gear, full trigger | 1/8 in. bit in steel, small bits in aluminum |
Big tools at low RPM need torque, so use low gear for any hole saw, any step drill past 1/2 in. and any bit over 3/8 in. in steel. An impact driver is fine for a hex-shank step drill in thin sheet. It is a poor fit for large holes in thick steel.
Why do drill bits overheat and turn blue?
Drill bits overheat and turn blue because too much of the drill's energy becomes heat instead of chips. The usual causes are too much speed, too little pressure, no cutting oil, and chips packed in the flutes. Blue is an oxide color: the steel surface got hot enough to change color, and the cutting edge itself was hotter still.
| What you see or hear | What it means | Fix |
|---|---|---|
| Blue or brown chips on steel | Speed too high for the bit | Drop to the chart speed and add cutting oil |
| Blue or straw color on the bit tip | The edge overheated and may have lost hardness | Resharpen past the colored part, or replace the bit |
| Squealing, no chips | Rubbing, not cutting | Push harder, slow down, add oil |
| Dust or fine powder instead of curls | Pressure too light or a dull bit | Push harder; if it still makes dust, sharpen |
| Smoke from the hole | Oil burning off: too fast or too dry | Slow down and use more oil |
| Stainless goes glassy and the bit stops cutting | The steel work-hardened from rubbing | Switch to cobalt, run slower and keep steady pressure |
| Bit binds and chips pack up | Flutes buried in the hole | Peck: back out every 1/2 in. or so to clear chips |
A good cut in steel makes a steady curl or ribbon of chip. If you are making dust, the bit is rubbing. Rubbing heats the edge faster than cutting does.
How does heat ruin a cutting tool?
Heat ruins a cutting tool by softening its edge. Once the edge softens, it wears fast, rubs instead of cutting and makes even more heat. That loop is why a bit can go from sharp to useless in a few holes.
| Tool material | How it handles heat | Best use | Our pick (1/4 in.) |
|---|---|---|---|
| High-speed steel (HSS) | Holds its hardness at the heat of normal drilling; softens if you let it run hot | Mild steel, aluminum, brass, wood | ThunderBit 012516, $3.24 each, sold in 12s |
| Cobalt (HSS-Co, M35 or M42) | Keeps its edge at higher heat than plain HSS, all the way through | Stainless steel, hard alloys | Cobalt ThunderBit 013516, $7.80 each, sold in 12s |
| Carbide-tipped | Handles the most heat, but is brittle and cracks from shock | Cast iron, abrasive metals, in a drill press | CTJ.250, $16.77 each, sold in 4s |
Store prices on Sept 28, 2026. Our drill bits are priced per bit and sold by the sleeve.
Cobalt does not let you drill faster. It gives you more room for error when the heat builds, which is why it is the pick for stainless steel. A coating such as TiN or AlTiN helps with heat and wear, but only on the surface. Once you resharpen, the new edge is bare HSS.
Carbide needs one extra care: never dunk a hot carbide tool in water. The sudden temperature change can crack it. Keep coolant steady or leave it off.
How do I keep cutting tools cool?
Keep a cutting tool cool by running at the chart speed, pushing hard enough to make chips, using the right cutting fluid and clearing chips often. Each one takes heat away from the edge.
| Metal | Cutting fluid |
|---|---|
| Mild steel | Sulfur-based cutting oil |
| Stainless steel | Sulfur-based cutting oil, and plenty of it |
| Aluminum | Light oil, kerosene or a little WD-40 |
| Cast iron | Dry (the graphite in the iron lubricates the cut) |
| Brass | Dry |
Push, don't polish. Firm, steady pressure makes chips. Light pressure makes heat.
Peck deep holes. Back out every half inch or so to clear chips and let oil in.
Use the shortest bit that reaches. Leave about two bit diameters of flute outside the hole so chips and heat can escape. Our guide to drill bits for metal has a length table.
Drill a pilot hole for big bits. Over 1/2 in., a 1/8 in. or 3/16 in. pilot takes load off the big bit's center.
Keep tools sharp. A dull edge rubs, and rubbing is heat.
Don't stop and restart in stainless. Each restart rubs a harder layer in the bottom of the hole.
Drilling tile or stone instead of metal? Diamond bits have their own heat rules. See our guide to drilling large holes in hard tile.
FAQ
Is it better to drill metal fast or slow?
Slow. Metal needs a lower speed than wood and firm pressure. Too much speed is the most common reason bits burn up in steel.
What RPM should I use for a 1/4 inch drill bit in steel?
About 1,400 RPM for an HSS bit in mild steel and about 600 RPM for a cobalt bit in stainless steel.
What speed should I drill stainless steel?
About 600 RPM for a 1/4 in. bit and 300 RPM for a 1/2 in. bit, with a cobalt bit, cutting oil and steady pressure.
What RPM for a 1/2 inch drill bit in steel?
About 700 RPM in mild steel, 550 RPM in cast iron and 300 RPM in stainless steel.
What is SFM?
SFM is surface feet per minute: how fast the cutting edge moves across the metal. Each metal has a good cutting speed, and the RPM formula turns it into a spindle speed for a given tool size.
Can I use an impact driver to drill metal?
Yes, for small holes and thin sheet with a hex-shank bit or step drill. For large holes or thick steel, use a drill in low gear or a drill press.
Can a blue drill bit be saved?
Often, yes. Grind the tip back past the discolored steel and resharpen it. If the blue runs far up the flutes, replace the bit.
Why does my hole saw keep burning up?
It is almost always spinning too fast. A 2 in. hole saw in steel wants about 150 RPM, which is low gear and a light trigger on a cordless drill. Use cutting oil and steady pressure.
Need a size that is not on these charts? Our drill size and decimal chart gives the decimal for every number, letter and metric size, ready for the RPM formula. Questions about a job? Call our team at (833) 4-ETOOLS or email sales@eldoradotools.com.
Rewritten Sept 28, 2026: new speed charts for drill bits, hole saws, step drills and countersinks. Prices checked on the store that day.