



















































Blog & Guides / Guides / Electrical
How to Choose Drill Bits for Metal (and Make Them Last)
How to choose drill bits for metal: HSS, cobalt or carbide, 118° vs 135° points, the right length for the hole, drilling speeds and price per bit.
Quick answer: The best drill bits for metal, for most jobs, are high-speed steel (HSS) jobber bits with a 135° split point and a black oxide or black and gold finish. For stainless steel, use cobalt. For cast iron and abrasive metal, use a carbide-tipped bit. Use bright (uncoated) HSS with a 118° point for aluminum and brass. Pick the shortest bit that leaves about two bit diameters of flute outside the hole. Run slow and steady with cutting oil: about 1,400 RPM for a 1/4 in. bit in mild steel and 600 RPM in stainless.
What drill bit should I use for metal?
A drill bit for metal is a twist drill made of high-speed steel, cobalt or carbide, with a cone-shaped point of 118° or 135°. You choose one by four things: what the bit is made of, its finish, its point angle and its length. This table gives our pick for each common metal, priced at the 1/4 in. size.
Metal to drill |
Bit to use |
Point |
Our pick (1/4 in.) |
Price per bit |
|---|---|---|---|---|
Mild steel, angle iron, strut, sheet metal |
Heavy-duty HSS, black and gold |
135° split |
$3.24, sold in 12s |
|
Same, on a budget |
HSS, black oxide |
135° split |
$2.60, sold in 12s (min. 24) |
|
Stainless steel, hard alloys |
Cobalt (HSS-Co) |
135° split |
$7.80, sold in 12s |
|
Cast iron, cast steel, bronze, hard copper |
Carbide-tipped |
118° |
$16.77, sold in 4s |
|
Steel and cast iron, longer life than oxide |
HSS with TiN (titanium) coating |
135° split |
$5.68, sold in 12s |
|
Aluminum, brass, copper, plastic |
Bright (uncoated) HSS |
118° |
$2.27, sold in 12s (min. 24) |
|
Metal, with an impact driver |
TiN HSS, 1/4 in. hex shank |
135° split |
$6.88, sold in 12s |
Store prices on Sept 27, 2026. Our drill bits are priced per bit and sold by the sleeve, usually 6 or 12.
If you only buy one kind, buy a 135° split-point, heavy-duty HSS jobber bit. It drills mild steel, iron, aluminum, wood and PVC, in a hand drill or a drill press. Browse every size in our high-speed drill bit collection.
What is the best drill bit for stainless steel?
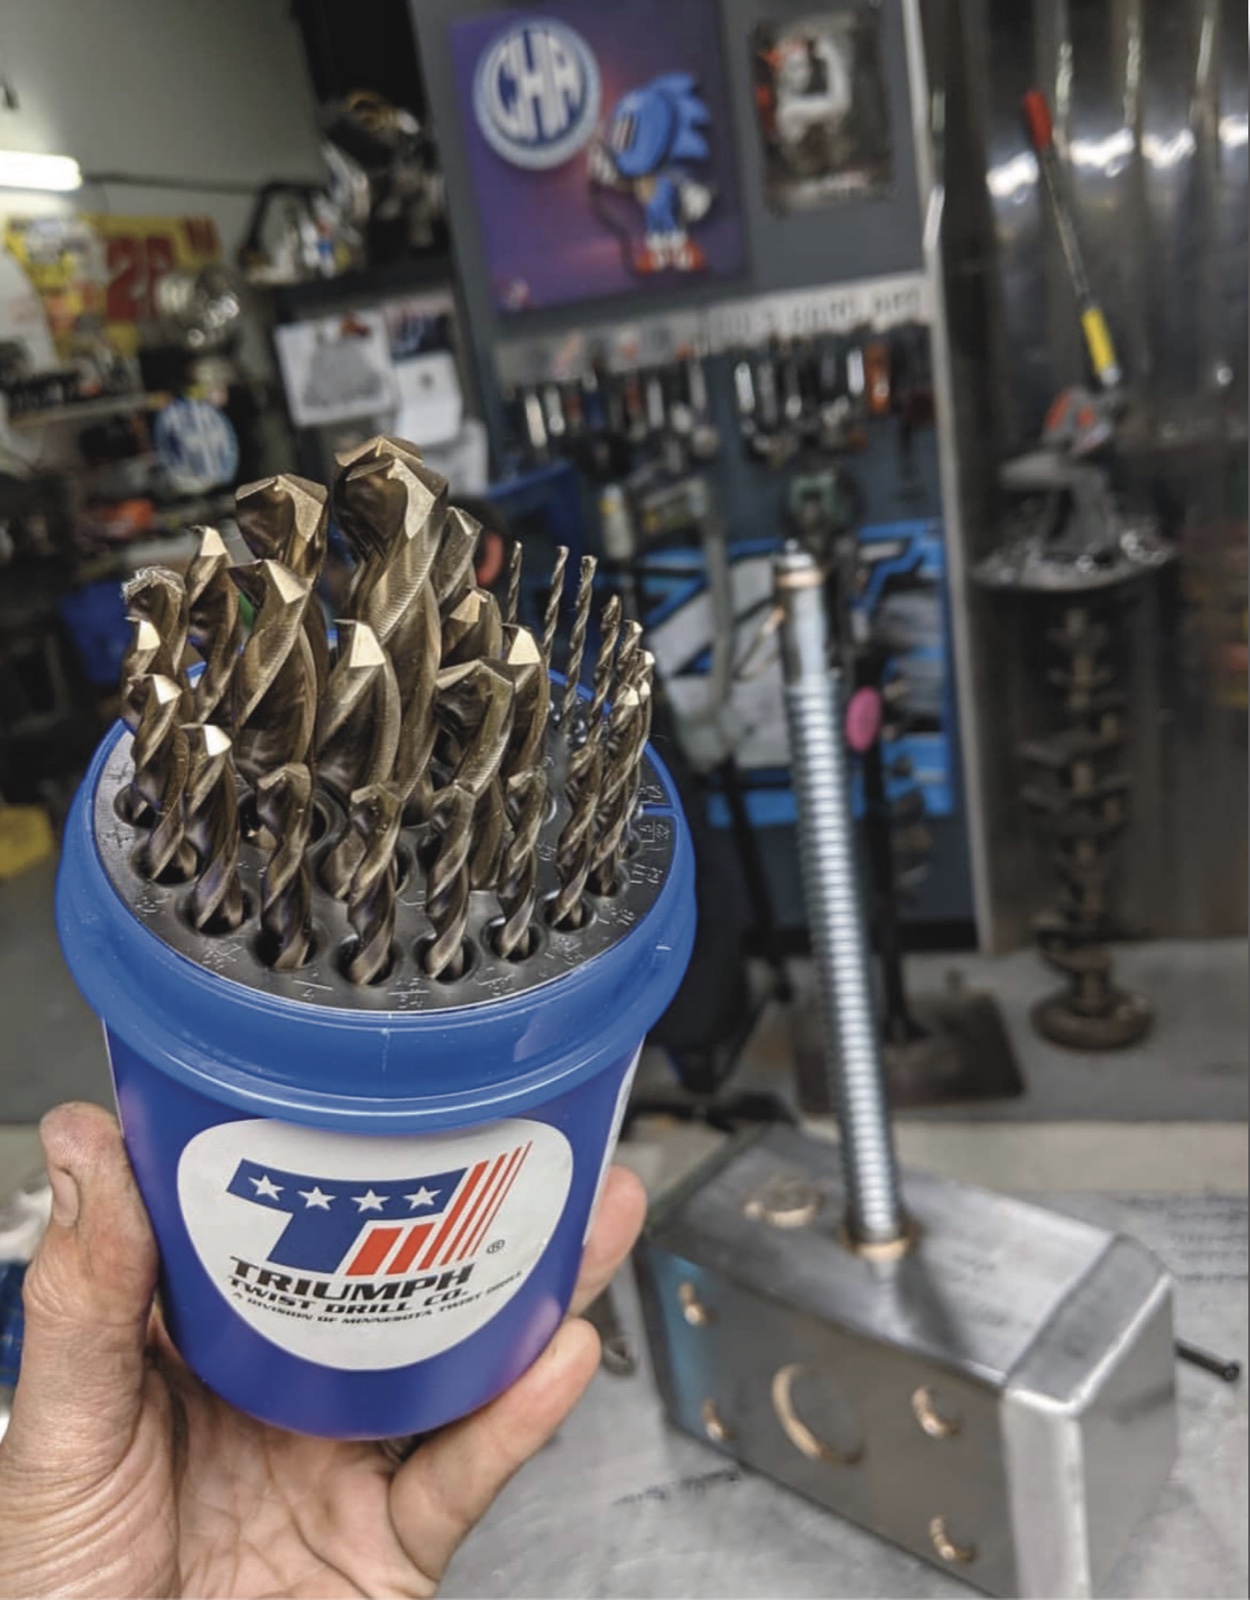
The best drill bit for stainless steel is a cobalt bit with a 135° split point. Cobalt bits are HSS with 5–8% cobalt mixed through the whole alloy (grades M35 and M42). The cobalt keeps the cutting edge hard at the high heat stainless makes. Plain HSS softens and dulls in a few holes.
Technique matters as much as the bit in stainless steel. Stainless work-hardens: if the bit rubs instead of cutting, the surface under the tip gets harder than the bit.
Run slow. About 600 RPM for a 1/4 in. bit, and about 300 RPM for 1/2 in.
Push hard and steady. The bit should make a curl of chip, not dust. Never let it spin in place.
Use cutting oil. A few drops on every hole cut heat and add life.
Do not stop and restart in the same hole. Each restart rubs a hard layer in the bottom of the hole.
Cobalt, titanium or black oxide: which drill bit is worth it?
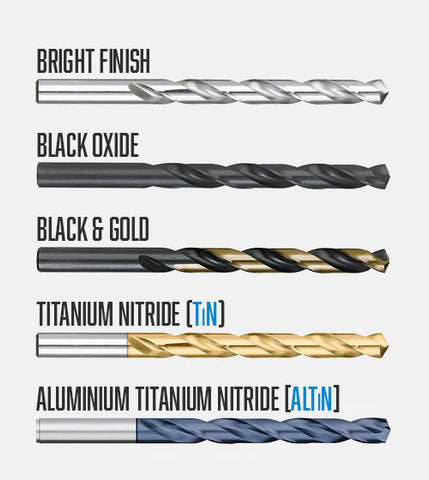
A cobalt drill bit is worth the extra cost in stainless and hard alloys. A titanium (TiN) bit is worth it for heavy use in mild steel and cast iron. Black oxide and black and gold bits are the best value for everyday steel. All four start as high-speed steel. What differs is the alloy and the coating.
Bit type |
What it is |
Best for |
1/4 in. price per bit |
|---|---|---|---|
Bright (uncoated) HSS |
Plain HSS with a polished surface. Chips do not stick to it. |
Aluminum, brass, copper, plastic, wood |
$2.27 (JL.250BR) |
Black oxide HSS |
HSS with a dark oxide layer that holds oil and resists rust |
Mild steel, iron |
|
Black and gold HSS |
Black oxide body with a gold (bronze) oxide tip for a tougher edge |
All-around steel work |
$3.24 (012516) |
Titanium (TiN) HSS |
M2 HSS with a hard, gold ceramic coating on the surface |
Heavy use in mild steel and cast iron |
$5.68 (012816) |
Cobalt (HSS-Co) |
HSS alloyed with 5–8% cobalt all the way through |
Stainless steel, hard alloys, high heat |
$7.80 (013516) |
Carbide-tipped |
HSS body with a brazed carbide cutting tip |
Cast iron, abrasive metal, in a rigid setup |
$16.77 (CTJ.250) |
Do the math by the hole, not by the bit. A cobalt bit costs about 2.4 times as much as a black and gold ThunderBit ($7.80 vs $3.24). In stainless steel, where plain HSS may stop cutting after a few holes, cobalt easily makes that up. In mild steel, the cheaper bit usually wins.
A titanium coating is only on the surface. Once you resharpen a TiN bit, the new cutting edge is plain HSS. A cobalt bit is the same metal all the way through, so it keeps its edge after sharpening.
Triumph rates its ThunderBits to drill up to 8 times as many holes as a standard general-purpose bit. The tapered web gets thicker toward the shank, which is why they snap less in a hand drill.
What length drill bit do I need?
Use the shortest drill bit that leaves about two bit diameters of flute outside the hole. The flutes are the spiral grooves. They carry chips and heat up and out. If the flutes are buried in the hole, chips pack in, heat builds and the bit dies early.
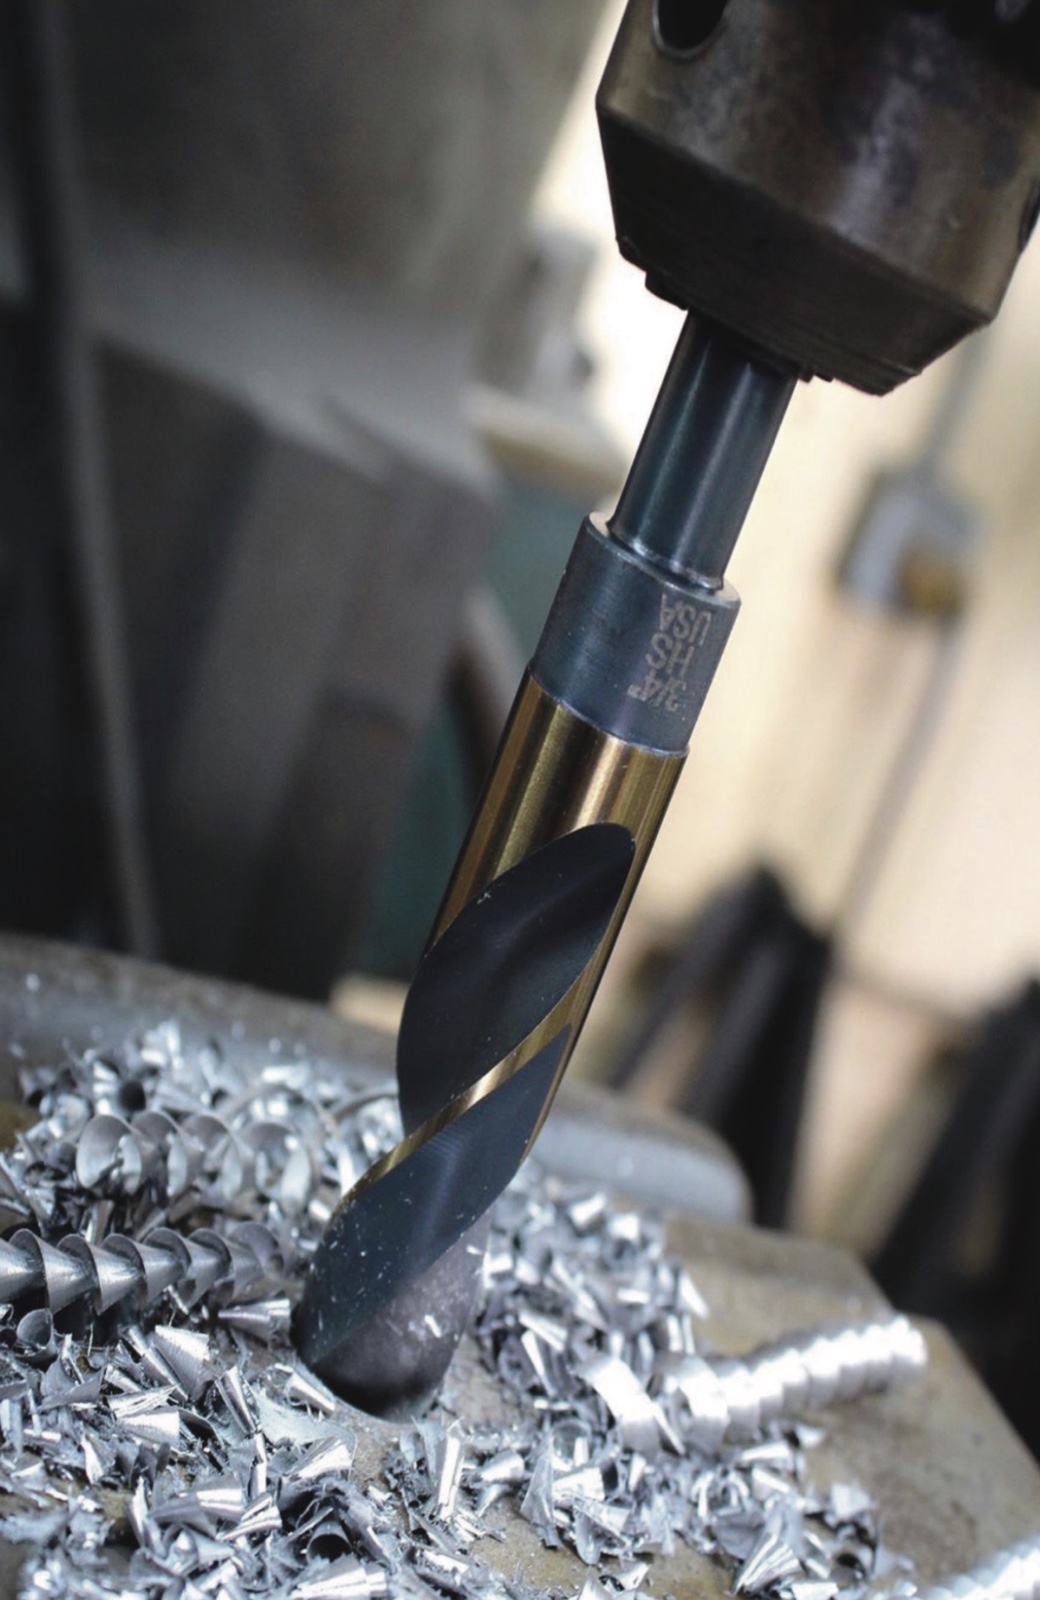
"Leave about twice the bit's diameter of flute sticking out of the hole. That gives the chips, the dust and the heat a way out. Bury the flutes and all of it gets trapped, and the bit dies a lot sooner."
David Castro, President, Eldorado Tools
So the deepest hole a bit should drill is its flute length minus two diameters. This table applies that rule to our own flute lengths.
Bit size |
Stubby: flute / deepest hole |
Jobber: flute / deepest hole |
12 in. aircraft (9 in. flute): deepest hole |
|---|---|---|---|
1/8 in. |
7/8 in. / 5/8 in. |
1-5/8 in. / 1-3/8 in. |
8-3/4 in. |
3/16 in. |
1-1/8 in. / 3/4 in. |
2-5/16 in. / 1-15/16 in. |
8-5/8 in. |
1/4 in. |
1-3/8 in. / 7/8 in. |
2-3/4 in. / 2-1/4 in. |
8-1/2 in. |
5/16 in. |
1-5/8 in. / 1 in. |
3-3/16 in. / 2-9/16 in. |
8-3/8 in. |
3/8 in. |
1-13/16 in. / 1-1/16 in. |
3-5/8 in. / 2-7/8 in. |
8-1/4 in. |
7/16 in. |
2-1/16 in. / 1-3/16 in. |
4-1/16 in. / 3-3/16 in. |
8-1/8 in. |
1/2 in. |
2-1/4 in. / 1-1/4 in. |
4-1/2 in. / 3-1/2 in. |
8 in. |
Flute lengths from our Triumph HD stubby (T4HD), HD jobber (T1D) and 118° aircraft extension (T1290) bits.
Example: a 2 in. deep hole with a 1/4 in. bit needs a jobber, because a stubby tops out at 7/8 in. A 1/2 in. deep hole in 1/4 in. plate is a stubby job. The shorter bit is stiffer, so it walks less and snaps less.
Stubby (screw machine) length: the stiffest bit. Best for sheet metal, thin plate, tight spaces and CNC work. See stubby drill bits, such as the 060416 at $3.00 each.
Jobber length: the standard length in most sets. Right for most holes in a drill press or hand drill.
6 in. and 12 in. HD extension bits: a jobber-length flute on a longer shank. They add reach past a flange or through a frame, not hole depth. See the 057516 (6 in., $5.90 each) and 058516 (12 in., $10.75 each).
Long-flute aircraft extension bits: a 9 in. flute on a 12 in. bit, or 13 in. on 18 in. These drill deep holes. See the 059816 (1/4 x 12 in., $31.68) and extra-length bits.
Should I use a 118° or 135° drill bit point?
Use a 135° split point for steel, stainless and most metal work, and a 118° point for aluminum, brass, wood and plastic. The 135° point is flatter and stronger. The split point adds small cutting edges at the center, so the bit starts where you put it without a center punch or pilot hole.
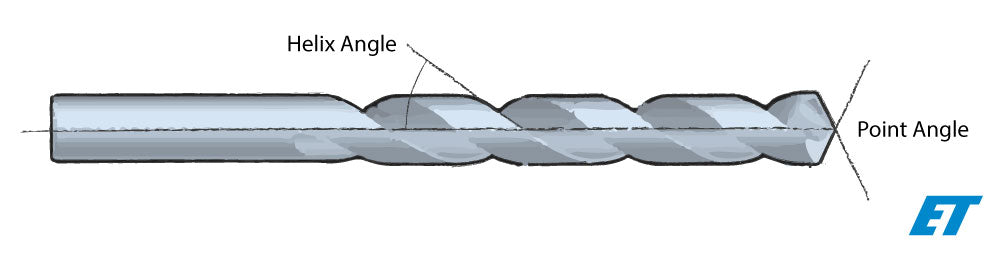
A 118° point is sharper, so it bites faster in soft metal. It walks more on hard or curved steel. That is why most heavy-duty bits, including all of our ThunderBits, use a 135° split point.
What speed should I drill metal at?
Drill metal slower than wood, and slower still as the bit gets bigger. A good starting speed is RPM = 3.82 × cutting speed ÷ bit diameter. The table uses common starting cutting speeds for HSS bits (cobalt for stainless).
Metal |
1/8 in. |
1/4 in. |
3/8 in. |
1/2 in. |
|---|---|---|---|---|
Aluminum |
7,650 RPM |
3,800 RPM |
2,550 RPM |
1,900 RPM |
Brass |
4,600 RPM |
2,300 RPM |
1,550 RPM |
1,150 RPM |
Mild steel |
2,750 RPM |
1,400 RPM |
900 RPM |
700 RPM |
Cast iron |
2,150 RPM |
1,050 RPM |
700 RPM |
550 RPM |
Stainless steel |
1,200 RPM |
600 RPM |
400 RPM |
300 RPM |
Starting cutting speeds used: aluminum 250, brass 150, mild steel 90, cast iron 70 and stainless 40 surface feet per minute.
Most cordless drills run about 400–600 RPM in low gear and 1,500–2,000 RPM in high. Use low gear for stainless steel and for any bit over 3/8 in. If the chips turn blue or the bit squeals, slow down. Our guide to proper RPM and overheating explains why heat is what kills drill bits.
Will these drill bits fit my drill?
Yes. A round-shank jobber bit up to 1/2 in. fits any 3/8 in. or 1/2 in. drill chuck, including DeWalt, Milwaukee, Makita, Ryobi and Bosch drills and drill presses. For other drivers, pick the shank to match.
Round shank: standard. Fits any 3-jaw chuck.
3-flat shank: three flats on the shank so the chuck jaws cannot slip. Good for high-torque cordless drills. See the ThunderBit+ 3-flat (12-pack, $41.57, about $3.46 per bit).
1/4 in. hex shank: snaps into an impact driver or quick-change chuck. See the 255HEX1664.
1/2 in. reduced shank (Silver and Deming): drills 9/16 in. to 1-1/4 in. holes with a 1/2 in. chuck. See Silver and Deming bits.
Need a size that is not a fraction, such as a #29 or letter F? Our drill size and tap drill chart lists every number, letter and metric size with its decimal.
How do I make drill bits last longer in metal?
Most drill bits for metal die from heat, not wear. Keep the speed down, keep steady pressure on the bit, use cutting oil, and clear chips from deep holes.
Let the bit cut. Firm pressure makes chips. Light pressure makes the bit rub, heat and dull.
Use cutting oil on steel and stainless. Aluminum can use oil or a little WD-40. Cast iron and brass drill dry.
Peck deep holes. Back the bit out every half inch or so to clear chips.
Clamp the work. A spinning part can cut you and snaps bits.
Drill a pilot for big holes. Over 1/2 in., a 1/8 in. or 3/16 in. pilot makes the big bit cut easier.
Ease off at breakthrough. The bit grabs as it exits thin metal. Back off pressure near the end.
Troubleshooting
Problem |
Likely cause |
Fix |
|---|---|---|
Bit walks off the mark |
118° point on hard or curved steel |
Use a 135° split point, or center punch first |
Bit dulls fast or turns blue |
Speed too high, not enough pressure, no oil |
Drop the RPM (see the speed table), push harder, add cutting oil |
Bit squeals and stops cutting in stainless |
The steel work-hardened from rubbing |
Switch to cobalt, run slower, and keep the bit cutting |
Chips pack and the bit binds |
Flutes buried in the hole |
Use a longer bit so two diameters of flute stay outside, and peck |
Bit snaps |
Bit too long, side load, or grabbing at breakthrough |
Use the shortest bit that reaches, and ease off at the end |
Hole is oversize or not round |
Worn point or bit wobble |
Resharpen or replace, and use a stubby for accuracy |
FAQ
How can I tell if a drill bit is for metal?
A drill bit for metal has a plain cone-shaped point of 118° or 135°, and the shank is usually marked HSS, Co, M35 or M42. A wood bit has a sharp center spur (brad point) or a flat paddle. A masonry bit has a flat carbide tip that is wider than the body.
What color drill bits are for metal?
Color is a finish, not a grade. Black oxide, black and gold, gold (TiN) and bronze (cobalt) bits are all made for metal. Bright silver bits are plain HSS, which drills soft metal fine. Check the markings, not just the color.
Are titanium drill bits good for metal?
Yes. A titanium drill bit is HSS with a titanium nitride (TiN) coating. It lasts longer than black oxide in mild steel and cast iron. For stainless steel, cobalt is the better choice.
What is the strongest drill bit for metal?
Carbide is the hardest, followed by cobalt, then HSS. Carbide is also brittle, so it needs a drill press or a rigid setup. For hand drilling in hard metal, cobalt is the strongest practical choice.
Do you need a special drill bit for metal?
Yes. Use a high-speed steel, cobalt or carbide twist drill. Wood bits and masonry bits will not cut steel. The good news is that a metal bit also drills wood and plastic.
What oil should I use for drilling metal?
Use a sulfur-based cutting oil on steel and stainless. Aluminum can take a light oil or a little WD-40. Cast iron and brass are usually drilled dry.
Where are these drill bits made?
Nearly every bit in our high-speed drill bit collection is made in the USA, mostly by Triumph Twist Drill and Tru-Cut.
For the bigger picture of drill bit types, from wood to masonry, see Drill Bits 101. Questions about a job? Call our team at (833) 4-ETOOLS or email sales@eldoradotools.com.
Published Sept 27, 2026. Prices checked on the store that day.