
































































































































































HomeBlog & GuidesGuidesMetal Fabrication
Carbide Burr Shapes Chart: Match Head to Cut (SA to SN)
Pick a carbide burr by the cut in front of you. An SA to SN chart with every head, size, price and max RPM, plus when a set beats singles.
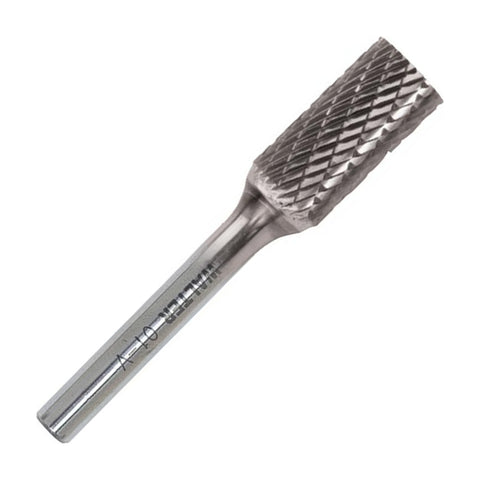
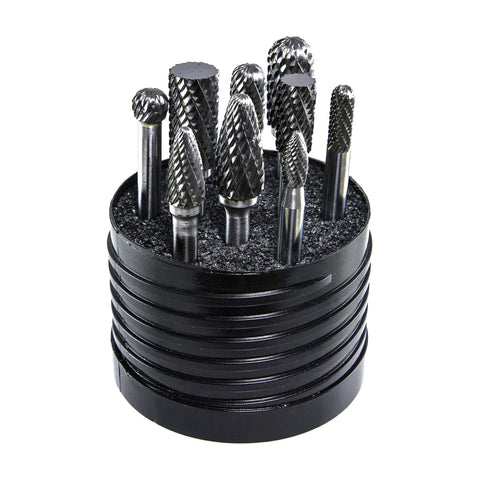
Quick answer: Pick a carbide burr shape by the metal you want gone. A flat weld crown takes a cylinder (SA-5). A fillet in an inside corner takes a round-nose tree (SF-5). A bevel takes a 14° cone (SL-4), a crack takes a ball (SD-5), and the back of a hole takes an inverted cone (SN). Use double cut on steel, stainless and cast iron. If you will use four or more shapes, a Drillco 8-piece set ($301.11, 1/2 in. heads, USA) costs less than four Walter singles.
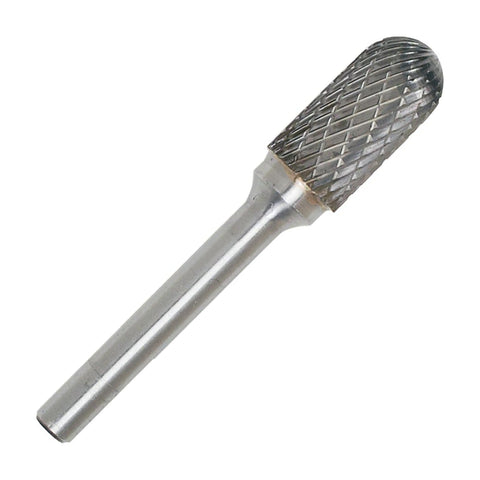
Look at the metal first. Inside corner: round nose. Flat crown: straight side. Bad spot in the bead: ball. The burr comes second. A carbide burr has the name it has because of the shape it leaves behind, so the head you pick should already look like the finished cut. People also call these die grinder bits, burr bits, rotary files and tungsten carbide burrs. They all mean the same tool: a solid carbide cutting head on a steel shank, run fast in a die grinder.
What are the carbide burr shapes, SA to SN?
Carbide burr shapes are 13 standard head profiles, each named with a two-letter code from SA to SN, and the shape of the head sets the shape of the cut. There is no SI. The S is the same on every code, so the second letter is the one to read. Some catalogs use their own single letters, so match the drawing or the head name when you cross over from another brand.
We stock 12 of the 13. The one we do not carry is SJ, the 60° countersink. Here is the carbide burr shape chart for our double cut burrs on a 1/4 in. shank.
Code |
Head |
What it is for |
Head diameters |
Price each |
|---|---|---|---|---|
SA |
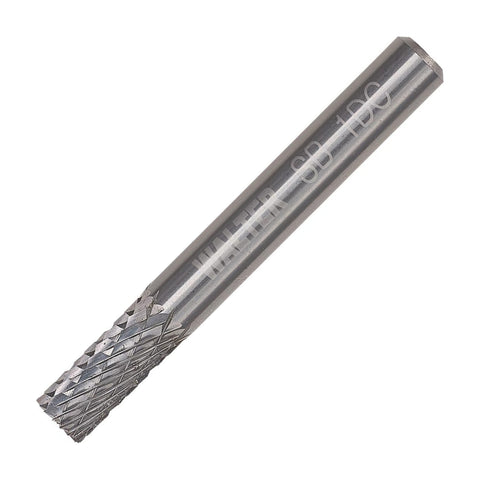
Cylinder, no end cut |
Flat faces and weld crowns. The end does not cut, so it can ride a wall without digging. |
1/4, 5/16, 3/8, 7/16, 1/2, 5/8 in. |
$44.18 to $92.02 |
SB |
Cylinder, end cut |
Square shoulders and flat bottoms. The end cuts, so it digs if you lean on it. |
1/4, 3/8, 1/2 in. |
$29.97 to $51.15 |
SC |
Cylinder, ball nose |
A flat that runs into a radius. Weld toes along a wall. |
1/4, 5/16, 3/8, 7/16, 1/2, 5/8, 3/4 in. |
$48.12 to $129.08 |
SD |
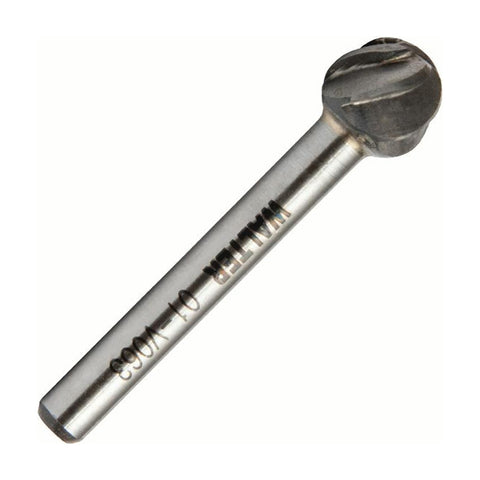
Ball |
Scooped pockets, weld defects, cross-drilled holes. |
1/4, 3/8, 1/2, 5/8 in. |
$47.22 to $87.46 |
SE |
Oval or egg |
A broad, open weld face. Long sweep, no flat spots. |
3/8, 1/2 in. |
$59.31 to $88.22 |
SF |
Tree, round nose |
Fillet welds and inside corners. The usual weld-blending head. |
1/4, 5/16, 3/8, 7/16, 1/2, 5/8 in. |
$53.57 to $92.02 |
SG |
Tree, pointed |
Sharp inside corners and narrow V-grooves. |
1/4, 5/16, 3/8, 1/2 in. |
$92.02 |
SH |
Flame |
Long contours, ports and castings. |
5/16, 1/2 in. |
$63.86 to $122.88 |
SK |
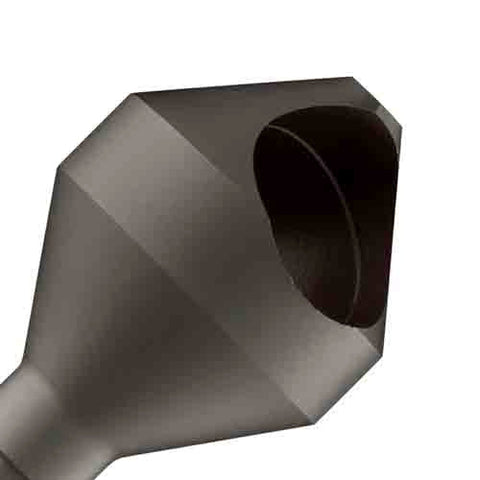
Countersink, 90° |
Chamfers and countersinks on a hole or edge. |
3/8, 1/2 in. |
$15.58 to $22.11 |
SL |
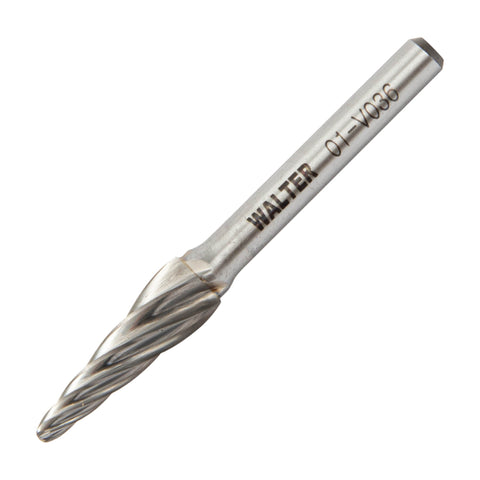
Cone, 14°, round nose |
Pipe and plate bevels, tapered slots, angled reach. |
1/4, 5/16, 3/8, 1/2, 5/8 in. |
$53.57 to $92.02 |
SM |
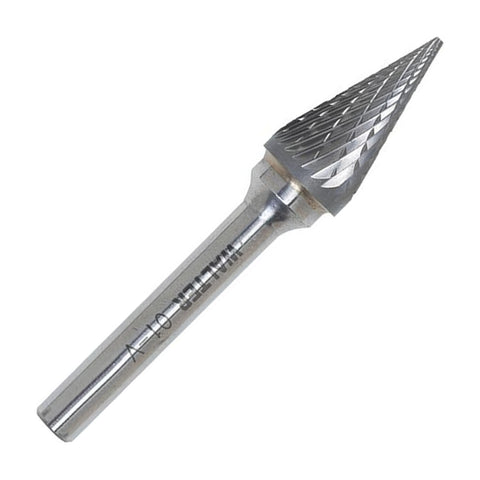
Cone, pointed |
Angled corners and tight points. |
1/4, 3/8, 1/2 in. |
$92.02 to $100.77 |
SN |
Inverted cone |
Back-side deburring and undercuts. |
1/4 in. |
$18.92 to $31.48 |
Prices checked in our catalog on Nov 9, 2026.
SA and SB look alike and cut differently. An SA has no teeth on the end, so it can ride against a wall. An SB has teeth on the end, so it squares a shoulder and will dig if you lean on it. The SB is also the bargain of the range: the 3/8 in. SB-3 is $29.97, about half the price of the SA-3 next to it at $59.31.
Which carbide burr shape do I need for this cut?
The carbide burr shape you need is the one that matches the cut you want to leave, so start from the joint, the edge or the defect in front of you. Find the job below and read across. All of these are Walter double cut burrs on a 1/4 in. shank, sold one at a time, for steel, stainless and cast iron.
The cut in front of you |
Head |
Code |
SKU |
Size |
Price each |
What the wrong head does |
|---|---|---|---|---|---|---|
Flush a weld crown on flat plate |
Cylinder, no end cut |
SA-5 |
1/2 x 1 in. |
$88.95 |
A round head leaves a row of scallops you then have to blend out. |
|
Square up a shoulder or flat bottom |
Cylinder, end cut |
SB-5 |
1/2 x 1 in. |
$51.15 |
An SA leaves a small uncut step in the corner. |
|
Blend a fillet weld in an inside corner |
Tree, round nose |
SF-5 |
1/2 x 1 in. |
$92.02 |
A pointed tree leaves a sharp groove at the root, which is a stress riser. |
|
Blend a weld toe along a straight wall |
Cylinder, ball nose |
SC-5 |
1/2 x 1 in. |
$100.77 |
A cylinder with a square edge undercuts the toe. |
|
Dress a wide, open weld face |
Oval or egg |
SE-5 |
1/2 x 7/8 in. |
$88.22 |
A small ball leaves grooves you can see after paint. |
|
Dig out a crack, pinhole or bad tack |
Ball |
SD-5 |
1/2 x 7/16 in. |
$66.11 |
A pointed head leaves a sharp-bottomed notch. |
|
Bevel plate or pipe for weld prep |
Cone, 14°, round nose |
SL-4 |
1/2 x 1-1/8 in. |
$87.46 |
A cylinder gives no bevel to follow. |
|
Clean a sharp corner or narrow V |
Tree, pointed |
SG-5 |
1/2 x 1 in. |
$92.02 |
A round-nose tree leaves metal in the corner. |
|
Chamfer or countersink a hole |
Countersink, 90° |
SK-5 |
1/2 x 1/4 in. |
$22.11 (min 2) |
A cone gives a 14° taper, which is the wrong angle for a flat-head screw. |
|
Deburr the back side of a hole or edge |
Inverted cone |
SN-1 |
1/4 x 1/2 in. |
$31.48 |
A forward cone cannot cut behind an edge at all. |
|
Shape a port or casting contour |
Flame |
SH-5 |
1/2 x 1-1/4 in. |
$122.88 |
A cylinder leaves steps along the curve. |
|
Get into an angled corner with a fine point |
Cone, pointed |
SM-5 |
1/2 x 7/8 in. |
$100.77 |
A round-nose cone cannot reach the last of the corner. |
Prices checked in our catalog on Nov 9, 2026.
Size follows the job. A burr too small for a fillet leaves steps you then have to chase out, so go as large as the corner lets you. A 1/2 in. head suits most structural fillets. Drop to 3/8 in. (SF-3, $62.18) when the walls are close. For a large fillet on heavy plate, the 5/8 in. SF-6 is $53.57, which is less than the 1/2 in. head.
Which die grinder bit is best for weld cleanup?
The best die grinder bits for weld cleanup are a round-nose tree for fillets, a cylinder for flat crowns and a ball for digging out defects. Those three heads handle most of what comes off a stinger. Bought singly at 1/2 in., SF-5, SA-5 and SD-5 come to $247.08. Add $54.03 and you can have those three plus five more heads in the Drillco set covered below.
A burr shapes the weld. It does not finish it. Once the profile is right, go to a flap disc for the blend (flap disc vs grinding wheel) or a wire cup brush for scale. The same die grinder also runs small cut-off wheels such as the 2-1/2 in. 11L263 ($4.13), covered in our cut-off wheel guide.
"Don't pick a burr by its name. Look at the joint. An inside corner wants a round nose, and a flat crown wants a straight side. Most gouges I've seen came from a pointed head doing a round-nose job."
David Castro, President, Eldorado Tools
What does the number in a carbide burr code mean?
The number in a carbide burr code usually marks the head diameter, but only on the straight shapes. On cylinders, balls and trees, 1 is 1/4 in., 3 is 3/8 in., 5 is 1/2 in. and 6 is 5/8 in. On cones, flames and inverted cones the number does not follow that ladder, so an SL-4 is 1/2 in. while an SA-4 is 7/16 in.
Family |
Code = head diameter x length of cut |
What the digit does |
|---|---|---|
SA |
SA-1 = 1/4 x 5/8 in., SA-2 = 5/16 x 3/4 in., SA-3 = 3/8 x 3/4 in., SA-4 = 7/16 x 1 in., SA-5 = 1/2 x 1 in., SA-6 = 5/8 x 1 in. |
Digit follows size |
SF |
SF-1 = 1/4 x 5/8 in., SF-2 = 5/16 x 5/8 in., SF-3 = 3/8 x 3/4 in., SF-4 = 7/16 x 1 in., SF-5 = 1/2 x 1 in., SF-6 = 5/8 x 1 in. |
Digit follows size |
SL |
SL-1 = 1/4 x 5/8 in., SL-2 = 5/16 x 7/8 in., SL-3 = 3/8 x 1-1/16 in., SL-4 = 1/2 x 1-1/8 in., SL-5 = 5/8 in. |
4 means 1/2 in. |
SH |
SH-3 = 5/16 x 3/4 in., SH-5 = 1/2 x 1-1/4 in. |
3 means 5/16 in. |
SM |
SM-1 = 1/4 x 1/2 in., SM-2 = 1/4 x 3/4 in., SM-3 = 1/4 x 1 in., SM-4 = 3/8 x 5/8 in., SM-5 = 1/2 x 7/8 in. |
1, 2 and 3 are all 1/4 in. |
SN |
SN-1 = 1/4 x 1/2 in., SN-2 = 1/4 x 3/4 in., SN-4 = 1/4 x 1 in. |
All 1/4 in.; digit sets length |
Two more marks turn up on the label. A two-digit number such as SA-43 or SF-42 means a miniature burr on a 1/8 in. shank. L6 means a 6 in. overall length. When you are matching a worn burr, measure the head with calipers and read the shape off the drawing. Do not trust the digit alone.
What sizes do carbide burrs come in?
Carbide burrs come in head diameters from 1/8 to 3/4 in. here, on 1/8 or 1/4 in. shanks. A 1/4 in. shank fits a standard air or electric die grinder. This is every double cut head we sell on that shank, with its maximum speed.
Code |
Head |
Diameter (in.) |
Length of cut (in.) |
SKU |
Price each |
Max RPM |
|---|---|---|---|---|---|---|
SA-1 |
Cylinder, no end cut |
1/4 |
5/8 |
$44.18 |
70,000 |
|
SA-2 |
Cylinder, no end cut |
5/16 |
3/4 |
$92.02 |
68,000 |
|
SA-3 |
Cylinder, no end cut |
3/8 |
3/4 |
$59.31 |
66,000 |
|
SA-4 |
Cylinder, no end cut |
7/16 |
1 |
$92.02 |
58,000 |
|
SA-5 |
Cylinder, no end cut |
1/2 |
1 |
$88.95 |
50,000 |
|
SA-6 |
Cylinder, no end cut |
5/8 |
1 |
$70.05 |
40,000 |
|
SB-1 |
Cylinder, end cut |
1/4 |
5/8 |
$33.12 |
70,000 |
|
SB-3 |
Cylinder, end cut |
3/8 |
3/4 |
$29.97 |
66,000 |
|
SB-5 |
Cylinder, end cut |
1/2 |
1 |
$51.15 |
50,000 |
|
SC-1 |
Cylinder, ball nose |
1/4 |
5/8 |
$48.12 |
70,000 |
|
SC-2 |
Cylinder, ball nose |
5/16 |
3/4 |
$92.02 |
68,000 |
|
SC-3 |
Cylinder, ball nose |
3/8 |
3/4 |
$65.35 |
66,000 |
|
SC-4 |
Cylinder, ball nose |
7/16 |
1 |
$92.02 |
58,000 |
|
SC-5 |
Cylinder, ball nose |
1/2 |
1 |
$100.77 |
50,000 |
|
SC-6 |
Cylinder, ball nose |
5/8 |
1 |
$65.35 |
40,000 |
|
SC-7 |
Cylinder, ball nose |
3/4 |
1 |
$129.08 |
— |
|
SD-1 |
Ball |
1/4 |
7/32 |
$47.22 |
70,000 |
|
SD-3 |
Ball |
3/8 |
5/16 |
$48.12 |
66,000 |
|
SD-5 |
Ball |
1/2 |
7/16 |
$66.11 |
50,000 |
|
SD-6 |
Ball |
5/8 |
9/16 |
$87.46 |
40,000 |
|
SE-3 |
Oval or egg |
3/8 |
5/8 |
$59.31 |
66,000 |
|
SE-5 |
Oval or egg |
1/2 |
7/8 |
$88.22 |
50,000 |
|
SF-1 |
Tree, round nose |
1/4 |
5/8 |
$92.02 |
70,000 |
|
SF-2 |
Tree, round nose |
5/16 |
5/8 |
$92.02 |
68,000 |
|
SF-3 |
Tree, round nose |
3/8 |
3/4 |
$62.18 |
66,000 |
|
SF-4 |
Tree, round nose |
7/16 |
1 |
$92.02 |
58,000 |
|
SF-5 |
Tree, round nose |
1/2 |
1 |
$92.02 |
50,000 |
|
SF-6 |
Tree, round nose |
5/8 |
1 |
$53.57 |
40,000 |
|
SG-1 |
Tree, pointed |
1/4 |
5/8 |
$92.02 |
70,000 |
|
SG-2 |
Tree, pointed |
5/16 |
3/4 |
$92.02 |
68,000 |
|
SG-3 |
Tree, pointed |
3/8 |
3/4 |
$92.02 |
66,000 |
|
SG-5 |
Tree, pointed |
1/2 |
1 |
$92.02 |
50,000 |
|
SH-3 |
Flame |
5/16 |
3/4 |
$63.86 |
68,000 |
|
SH-5 |
Flame |
1/2 |
1-1/4 |
$122.88 |
50,000 |
|
SK-3 |
Countersink, 90° |
3/8 |
— |
$15.58 (min 2) |
66,000 |
|
SK-5 |
Countersink, 90° |
1/2 |
1/4 |
$22.11 (min 2) |
50,000 |
|
SL-1 |
Cone, 14°, round nose |
1/4 |
5/8 |
$53.57 |
70,000 |
|
SL-2 |
Cone, 14°, round nose |
5/16 |
7/8 |
$92.02 |
68,000 |
|
SL-3 |
Cone, 14°, round nose |
3/8 |
1-1/16 |
$73.22 |
66,000 |
|
SL-4 |
Cone, 14°, round nose |
1/2 |
1-1/8 |
$87.46 |
50,000 |
|
SL-5 |
Cone, 14°, round nose |
5/8 |
— |
$92.02 |
40,000 |
|
SM-1 |
Cone, pointed |
1/4 |
1/2 |
$92.02 |
70,000 |
|
SM-2 |
Cone, pointed |
1/4 |
3/4 |
$92.02 |
70,000 |
|
SM-3 |
Cone, pointed |
1/4 |
1 |
$92.02 |
70,000 |
|
SM-4 |
Cone, pointed |
3/8 |
5/8 |
$92.02 |
66,000 |
|
SM-5 |
Cone, pointed |
1/2 |
7/8 |
$100.77 |
50,000 |
|
SN-1 |
Inverted cone |
1/4 |
1/2 |
$31.48 |
70,000 |
|
SN-2 |
Inverted cone |
1/4 |
3/4 |
$18.92 (min 2) |
70,000 |
|
SN-4 |
Inverted cone |
1/4 |
1 |
$24.51 (min 2) |
70,000 |
Prices checked in our catalog on Nov 9, 2026.
Three smaller ranges cover special cases. A 6 in. long shank burr reaches inside tube, tanks and deep weld prep, where the grinder body would hit first. A miniature burr on a 1/8 in. shank handles small radii and detail work. A hard alloy burr uses a harder carbide grade for hardened steel, high-nickel alloys and work-hardened stainless.
Code |
Head |
Line |
Diameter (in.) |
Length of cut (in.) |
SKU |
Price each |
Max RPM |
|---|---|---|---|---|---|---|---|
SA-1 |
Cylinder, no end cut |
6 in. long |
1/4 |
5/8 |
$92.02 |
35,000 |
|
SA-3 |
Cylinder, no end cut |
6 in. long |
3/8 |
3/4 |
$92.02 |
33,000 |
|
SA-5 |
Cylinder, no end cut |
6 in. long |
1/2 |
1 |
$92.02 |
25,000 |
|
SC-1 |
Cylinder, ball nose |
6 in. long |
1/4 |
5/8 |
$92.02 |
35,000 |
|
SC-3 |
Cylinder, ball nose |
6 in. long |
3/8 |
3/4 |
$92.02 |
33,000 |
|
SC-5 |
Cylinder, ball nose |
6 in. long |
1/2 |
1 |
$92.02 |
25,000 |
|
SD-1 |
Ball |
6 in. long |
1/4 |
7/32 |
$92.02 |
35,000 |
|
SD-3 |
Ball |
6 in. long |
3/8 |
5/16 |
$92.02 |
33,000 |
|
SD-5 |
Ball |
6 in. long |
1/2 |
7/16 |
$92.02 |
25,000 |
|
SF-1 |
Tree, round nose |
6 in. long |
1/4 |
5/8 |
$92.02 |
35,000 |
|
SF-3 |
Tree, round nose |
6 in. long |
3/8 |
3/4 |
$92.02 |
33,000 |
|
SF-5 |
Tree, round nose |
6 in. long |
1/2 |
1 |
$92.02 |
25,000 |
|
SG-1 |
Tree, pointed |
6 in. long |
1/4 |
5/8 |
$92.02 |
35,000 |
|
SG-3 |
Tree, pointed |
6 in. long |
3/8 |
3/4 |
$92.02 |
33,000 |
|
SG-5 |
Tree, pointed |
6 in. long |
1/2 |
1 |
$92.02 |
25,000 |
|
SL-3 |
Cone, 14°, round nose |
6 in. long |
3/8 |
1-1/16 |
$92.02 |
33,000 |
|
SL-5 |
Cone, 14°, round nose |
6 in. long |
5/8 |
— |
$92.02 |
20,000 |
|
SA-43 |
Cylinder, no end cut |
1/8 in. shank |
1/8 |
9/16 |
$23.60 (min 2) |
— |
|
SD-42 |
Ball |
1/8 in. shank |
1/8 |
1/8 |
$23.60 (min 2) |
— |
|
SF-42 |
Tree, round nose |
1/8 in. shank |
1/8 |
1/2 |
$23.60 (min 2) |
— |
|
SG-44 |
Tree, pointed |
1/8 in. shank |
1/8 |
1/2 |
$23.60 (min 2) |
— |
|
SL-42 |
Cone, 14°, round nose |
1/8 in. shank |
1/8 |
1/2 |
$23.60 (min 2) |
— |
|
SM-42 |
Cone, pointed |
1/8 in. shank |
1/8 |
7/16 |
$23.60 (min 2) |
— |
|
SC-5 |
Cylinder, ball nose |
Hard alloy |
1/2 |
1 |
$107.89 |
50,000 |
|
SF-5 |
Tree, round nose |
Hard alloy |
1/2 |
1 |
$99.28 |
50,000 |
|
SL-4 |
Cone, 14°, round nose |
Hard alloy |
1/2 |
1-1/8 |
$104.72 |
50,000 |
Prices checked in our catalog on Nov 9, 2026.
Is a carbide burr set cheaper than buying singles?
A carbide burr set is cheaper than buying singles once you need about four shapes. The Drillco No. 3 set holds eight 1/2 in. double cut heads for $301.11, made in the USA. Any four of those same shapes as Walter singles cost at least $330.74, and all eight cost $716.32. Below four heads, singles win.
Online you will also see no-name single burrs for $9 to $16. We do not stock that tier. If cost per burr is the deciding number, our answer is a Drillco set at $19.87 to $37.64 a burr. Drillco and Walter are different makers, so read the comparison as the same shapes and sizes, not the identical tool.
Set |
Set price ($) |
Same shapes as singles ($) |
|---|---|---|
70S011DC |
173.48 |
474.53 |
70S002DC |
203.29 |
551.53 |
70S003DC |
301.11 |
716.32 |
70S005DC |
322.51 |
806.19 |
01V990 |
402.49 |
404.91 |
Here is what each set holds and what it costs per burr.
Set |
Pieces |
Shank |
Holds |
Set price |
Per burr |
Same shapes singly |
Made in |
|---|---|---|---|---|---|---|---|
8, all 1/2 in. |
1/4 in. |
SA-5, SC-5, SD-5, SE-5, SF-5, SG-5, SL-4, SM-5 |
$301.11 |
$37.64 |
$716.32 |
USA |
|
8, all 3/8 in. |
1/4 in. |
SA-3, SC-3, SD-3, SE-3, SF-3, SG-3, SL-3, SM-4 |
$203.29 |
$25.41 |
$551.53 |
USA |
|
8, all 1/4 in. |
1/4 in. |
SA-1, SC-1, SD-1, SE-1, SF-1, SG-1, SL-1, SM-1 |
$158.95 |
$19.87 |
$469.15 (7 of 8) |
USA |
|
10, 3/8 to 1/2 in. |
1/4 in. |
SA-5, SC-3, SC-5, SD-5, SE-3, SF-3, SF-5, SG-3, SG-5, SL-4 |
$322.51 |
$32.25 |
$806.19 |
USA |
|
10, 1/4 to 1/2 in. |
1/4 in. |
SA-1, SA-3, SA-5, SC-1, SC-3, SC-5, SD-3, SF-3, SF-5, SH-1 |
$262.89 |
$26.29 |
$609.00 (9 of 10) |
USA |
|
5, all 1/2 in. |
1/4 in. |
SA-5, SC-5, SF-5, SG-5, SM-5 |
$173.48 |
$34.70 |
$474.53 |
USA |
|
5, 3/8 to 5/8 in. |
1/4 in. |
SA-3, SC-3, SD-6, SF-5, SM-5 |
$402.49 |
$80.50 |
$404.91 |
China |
Prices checked in our catalog on Nov 9, 2026.
The Walter kit is the exception. The five burrs in 01V990 cost $404.91 singly and $402.49 in the kit, so you save $2.42. Buy that kit for the case and one brand across the bench, not to save money. Drillco sets No. 1 through No. 5 also come in single cut at the same price. For 1/8 in. shanks, Drillco No. 6 gives you eight 1/8 in. heads for $70.77, or $8.85 a burr. Browse all of them in our carbide burr sets.
Which carbide burr should I use on stainless, cast iron and hardened steel?
Use a double cut carbide burr on stainless, cast iron and most hardened steel, and move to a hard alloy burr when the steel is hardened or high in nickel and a standard burr is wearing out. Double cut has two crossing sets of teeth that break the metal into small chips, which gives you more control. Single cut throws longer chips and removes metal more aggressively, but we sell it only inside the Drillco sets.
Material |
Cut |
Pick |
Watch for |
|---|---|---|---|
Mild and carbon steel |
Double cut |
Let the teeth cut. Pushing harder makes heat, not chips. |
|
Stainless |
Double cut |
Same head as for steel |
Keep the burr moving and cutting. Stainless hardens where a burr rubs. Keep a burr that has cut carbon steel off stainless that must resist rust. |
Cast iron |
Double cut |
Same head as for steel |
Abrasive and brittle at the edges. Single cut in a Drillco set is the option for heavy stock removal. |
Hardened steel, 45 to 60 Rc; high-nickel alloys |
Double cut, hard alloy grade |
01V034 SF-5, $99.28 |
A harder grade is also more brittle. Go straight into the work, no side loads. |
Aluminum, brass, copper |
Aluminum cut only |
A double cut burr clogs on soft metal within seconds. |
A broken bit stuck in a hole is a hard-material problem too, and our guide to drill bits for hardened steel covers the drilling side.
Why is my carbide burr chattering, chipping or leaving gouges?
A carbide burr usually chatters, chips or gouges because the head is wrong for the cut, too much shank is showing, or the burr is rubbing instead of cutting. The mark it leaves tells you which.
What you see |
Likely cause |
Fix |
|---|---|---|
Grinder bounces and chatters |
Burr rubbing, or a loose workpiece |
Clamp the work. Use steady pressure so the teeth bite. |
Chatter gets worse with reach |
Too much shank out of the collet |
Seat the shank as far as it will go, or move to a 6 in. burr rated for reach. |
Teeth chipped |
Side load, a dropped burr, or a coarse cut on hard metal |
Change to double cut. Use hard alloy on hardened steel, and go straight in. |
Gouge beside the weld |
An end-cut SB or a pointed head where a round nose belongs |
Change to an SA for flats or an SF for corners. |
Row of scallops |
Head too small, or a ball on a flat |
Go up a size, or change to a cylinder or oval. |
Head looks silver and smooth |
Aluminum packed into a double cut burr |
Use an aluminum cut burr. |
Head dulled and work gets hot |
Burr is worn out |
Replace it. A dull burr only makes heat. |
Wear eye and face protection every time. Carbide burrs throw hot, sharp chips, and a broken head can fly.
FAQ
How fast can I run a carbide burr?
Run a carbide burr below the maximum for its head size. Walter rates 1/4 in. heads at 70,000 RPM, 3/8 in. at 66,000, 1/2 in. at 50,000 and 5/8 in. at 40,000. Those are ceilings, not targets, and each 6 in. burr has its own lower rating in the table above.
Can you use a carbide burr in a drill?
No. A drill turns about 2,000 to 3,000 RPM, far too slow for a burr, so the teeth grab and chip. Use an air or electric die grinder.
Can I use a carbide burr in a Dremel?
Yes, if the burr has a 1/8 in. shank and your tool has a 1/8 in. collet. Our 1/4 in. shank burrs will not fit. Miniature burrs and the Drillco No. 6 set are the ones to look at.
What is a die grinder used for?
A die grinder is a handheld high-speed tool for burrs, small grinding wheels and small cut-off wheels. It is larger and stronger than a Dremel and usually takes a 1/4 in. shank. We carry one, the Walter DIALSPEED 6141 point grinder ($579.42), with six speeds from 10,000 to 30,500 RPM.
How long do carbide burrs last?
No fixed number holds, because the metal, the pressure and the speed all change the answer. A carbide burr is done when it stops throwing chips and starts making heat.
Will a carbide burr cut through a drill bit?
Yes. Carbide is harder than a high-speed steel drill bit, so a burr can grind one away. Use a small ball or pointed head and light pressure, because the broken bit is brittle.
Who makes the best carbide burrs?
We sell Walter and Drillco, so those are the two we can speak for. Drillco sets are made in the USA, and Walter 01V burrs are made in China and sold one at a time in the widest range of sizes. PFERD and SGS are other well-regarded makers that we do not carry.
What is the difference between single cut and double cut?
Single cut has one set of spiral teeth and throws long chips. Double cut, also called diamond cut or cross cut, has two crossing sets, leaves small chips and gives more control. Double cut is the default for steel and stainless.
What is a 6 in. carbide burr for?
A 6 in. burr reaches inside tube, tanks and deep weld prep. The long shank flexes, so maximum speed is about half that of a standard burr. Keep the feed light and check the rating for your head size.
Not sure which head fits the job? Call our team at (833) 4-ETOOLS or email sales@eldoradotools.com with a photo of the joint and the metal, and we will name the burr.
Related: deburring tools for metal for clean hole edges, counterbore vs countersink for seating screws, sanding discs for metal for the finish, and the full carbide burr range.
Sources: Walter and Drillco product specifications; retail prices as shown in Google AI Mode results on Nov 9, 2026.
First published [date], with prices checked in our catalog on Nov 9, 2026.